







Explosion Proof European Overhead Crane
Products Description
Key Features of Explosion-Proof European Overhead Cranes
1. Explosion-Proof Components
Hoist & Trolley: Certified motors, brakes, and controls that prevent sparks.
Electrical Systems: Flameproof enclosures, intrinsically safe circuits.
Wiring & Connections: Sealed conduits to prevent arc flashes.
2. ATEX & IECEx Compliance
Meets ATEX Directive 2014/34/EU (for EU) and IECEx (global).
Classified for Zone 1, Zone 2 (gases) or Zone 21, Zone 22 (dust).
3. Construction Materials
Non-sparking metals (stainless steel, aluminum alloys).
Anti-static coatings to prevent electrostatic discharge.
4. Special Safety Mechanisms
Thermal protection in motors to prevent overheating.
Emergency stop with explosion-proof buttons.
Spark-resistant brakes & gears.
5. Customization Options
Single or double girder designs.
Manual or remote control (intrinsically safe).
Load capacities from 1 ton to 100+ tons.
Comparison: Standard vs. Explosion-Proof Cranes
| Feature | Standard Crane | Explosion-Proof Crane |
|---|---|---|
| Certification | CE, ISO | ATEX, IECEx, EN 60079 |
| Electrical Safety | Standard enclosures | Flameproof (Ex d) or Intrinsic Safety (Ex i) |
| Materials | Carbon steel | Stainless steel, non-sparking alloys |
| Cost | Lower upfront cost | Higher (20–40% premium for Ex-rated parts) |
| Maintenance | Routine checks | Strict inspections for Ex compliance |
Comparison: Standard vs. Explosion-Proof Overhead Crane
| Feature | Standard Overhead Crane | Explosion-Proof Overhead Crane |
|---|---|---|
| Motor & Electricals | Standard, no special protection | Spark-proof, flameproof enclosures |
| Certification | CE, FEM, ISO | ATEX, IECEx, EN 60079 |
| Usage Environment | Normal industrial settings | Hazardous (Zone 1, Zone 2, Zone 21, Zone 22) |
| Cost | Lower | Higher (due to specialized components) |

Pictures & Components
An explosion-proof overhead crane designed for European markets (complying with ATEX/IECEx) consists of specialized components engineered to prevent ignition in hazardous environments (Zone 1, Zone 2, Zone 21, Zone 22). Below is a detailed breakdown of its critical components:
1. Explosion-Proof Bridge (Girder)
Made of non-sparking materials (e.g., stainless steel or coated steel).
Designed to minimize friction and static buildup.
Available in single-girder (light/medium duty) or double-girder (heavy-duty) configurations.

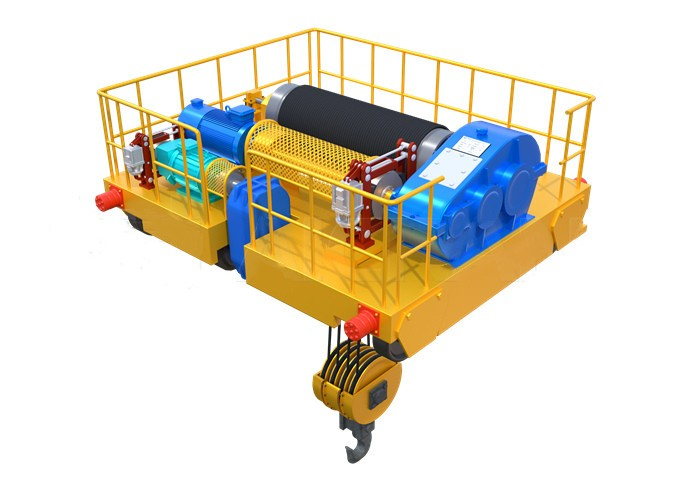
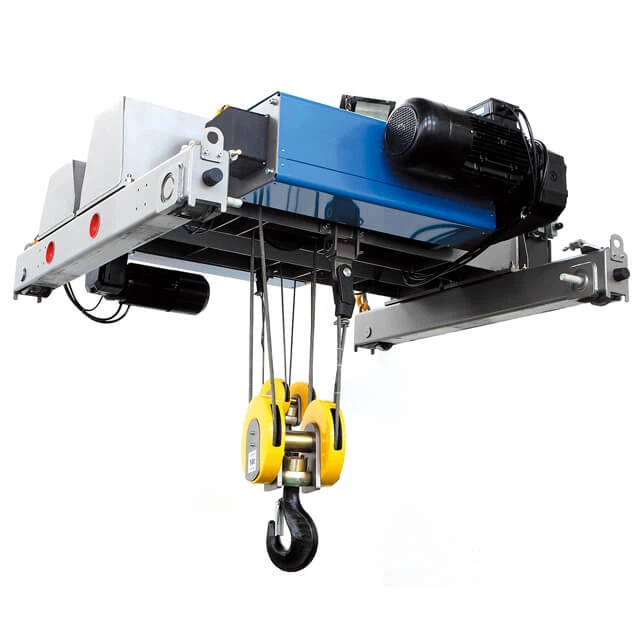
2. Explosion-Proof Hoist Unit
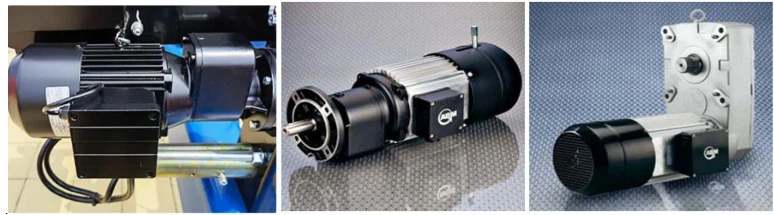
Motor:
ATEX-certified electric motor (Ex d, Ex e, or Ex nR rating).
Thermal protection to prevent overheating.
Braking System:
Spark-resistant brakes (mechanical or electromagnetic).
Fail-safe mechanisms for emergency stops.
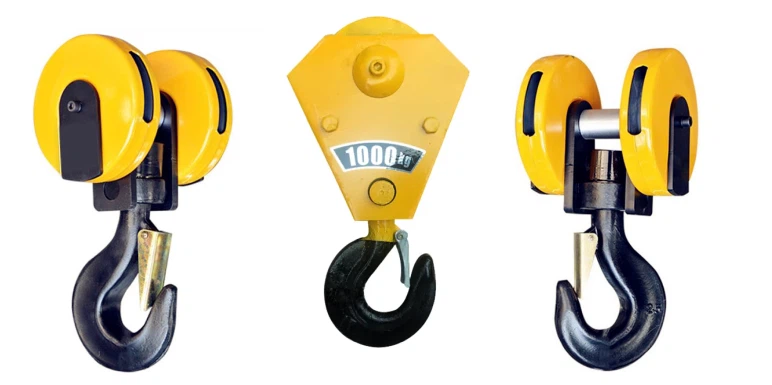
Lifting Mechanism:
Wire rope hoist (Ex-rated) or chain hoist (spark-resistant).
Hook & load block made of non-sparking alloys.
 |
 |
3. Explosion-Proof Trolley
Houses the hoist and moves along the bridge.
Wheels & bearings made of anti-static materials.
Motor & gearbox with flameproof enclosures (Ex d).
Limit switches with explosion-proof housing.
 |
 |
4. Explosion-Proof Electrical System
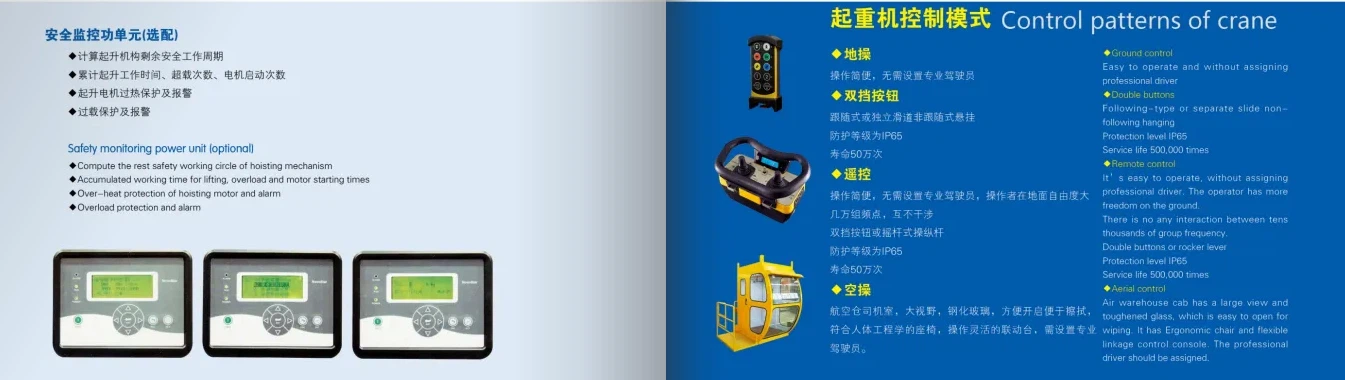
Control Panel:
Housed in flameproof (Ex d) or pressurized (Ex p) enclosures.
Includes overload relays, contactors, and circuit breakers rated for hazardous areas.
Wiring & Conduits:
Sealed, armored cables to prevent sparking.
Intrinsically safe (Ex i) circuits for low-voltage controls.
Festoon System / Cable Reel:
Spark-resistant cable management for power and signal transmission.
5. Explosion-Proof Runway & End Trucks
Runway Beams:
Steel or aluminum with anti-static coatings.
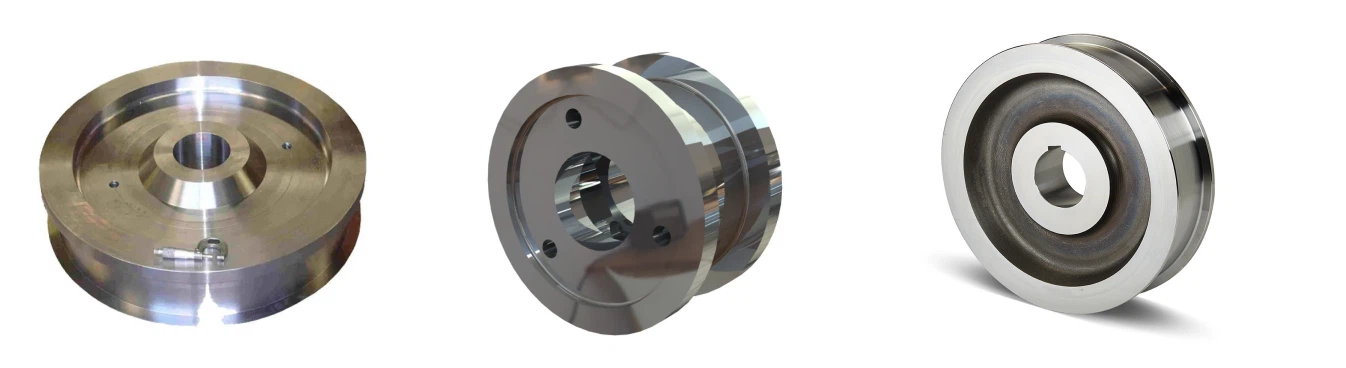
End Trucks (Wheel Assemblies):
Explosion-proof motors for travel movement.
Non-sparking wheels (bronze or polyurethane).
Rail & Guide System:
Grounded to prevent static discharge.
6. Explosion-Proof Controls
Pendant Control (Ex-rated):
ATEX-certified handheld controller with sealed buttons.
Radio Remote Control (Ex-approved):
Wireless operation with intrinsically safe signals.
Cab Control (if applicable):
Pressurized operator cabin for Zone 1 environments.

7. Safety & Monitoring Systems
Overload Protection:
ATEX-compliant load limiter.
Emergency Stop (Ex-rated):
Mushroom-style E-stop with explosion-proof housing.
Anti-Collision System:
Infrared or laser sensors with Ex-rated enclosures.
Temperature & Gas Sensors:
Monitors environmental conditions in real time.
.
8. Additional Explosion-Proof Features
Static Dissipation:
Conductive tires, grounding straps.
Corrosion Resistance:
Special coatings for chemical exposure.
Dust-Proofing (for Zone 21/22):
Sealed bearings, dust-tight enclosures.

Comparison: Standard vs. Explosion-Proof Components
| Component | Standard Crane | Explosion-Proof Crane |
|---|---|---|
| Motor | Standard IP55 | ATEX Ex d/Ex e Certified |
| Control Panel | Standard enclosure | Flameproof (Ex d) |
| Wiring | Normal insulation | Armored, sealed conduits |
| Brakes | Standard friction | Spark-resistant materials |
| Remote Control | Standard RF | Intrinsically Safe (Ex i) |

SKETCH

Main technical

Advantages
Enhanced Safety in Hazardous Areas
Certified for ATEX/IECEx standards, preventing sparks, arcs, or heat sources that could ignite flammable gases, vapors, or dust (Zones 1, 2, 21, 22).
Non-sparking materials (stainless steel, bronze) and anti-static coatings minimize explosion risks.
Compliance with Strict EU Regulations
Meets ATEX 2014/34/EU and EN 60079 standards for explosive atmospheres.
Required in industries like oil & gas, chemicals, and pharmaceuticals under EU safety laws.
Robust and Reliable Construction
Flameproof (Ex d) or pressurized (Ex p) enclosures for motors and electrical components.
Corrosion-resistant for harsh environments (e.g., offshore platforms, chemical plants).
Precision and Efficiency
Smooth operation with variable frequency drives (VFDs) for controlled acceleration.
Remote or pendant controls (Ex-rated) allow safe operation from a distance.
Reduced Downtime & Maintenance
Durable components (e.g., spark-resistant brakes, sealed bearings) extend service life.
Fewer safety incidents mean lower operational disruptions.
Customizable for Specific Hazards
Configurations for gas (Zone 1/2) or dust (Zone 21/22) environments.
Options include single/double girder, underhung, or top-running designs.
Application:
1. Oil & Gas
Refineries: Handling pipelines, valves, and explosive chemicals.
Offshore Rigs: Lifting equipment in methane-rich environments (Zone 1).
2. Chemical & Pharmaceutical
Solvent Processing: Transporting flammable liquids (e.g., ethanol, acetone).
Reactor Maintenance: Installing/removing explosion-prone machinery.
3. Mining & Coal Handling
Coal Silos: Operating in combustible dust (Zone 22).
Methane-Prone Tunnels: Equipment assembly in Zone 1 areas.
4. Food & Grain Processing
Flour Mills/Grain Silos: Preventing dust explosions (Zone 21).
Sugar Plants: Handling powdered ingredients.
5. Aerospace & Defense
Rocket Fuel Handling: Moving volatile propellants safely.
6. Paint & Coatings
Spray Booths: Operating near flammable vapors (Zone 2).
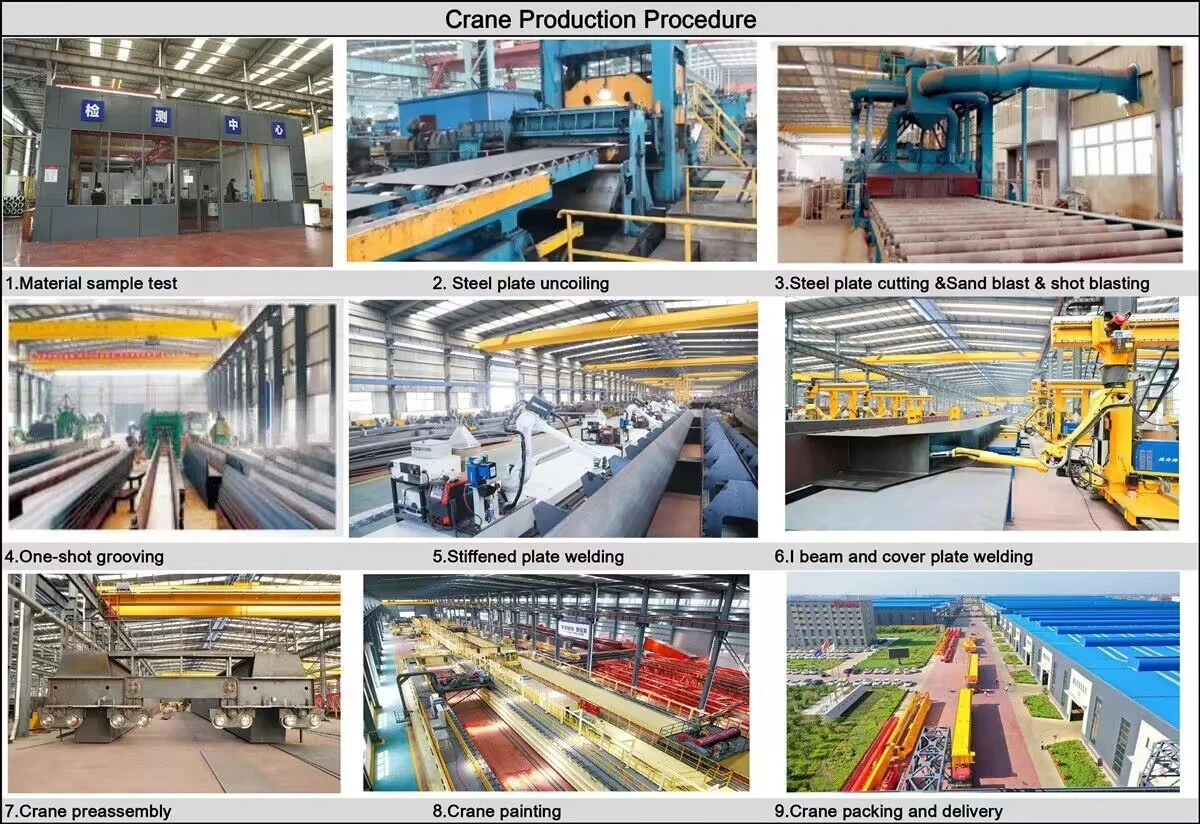
Crane production procedure
1.Design and Engineering
Requirements Gathering:
Load capacity (e.g., 10T, 50T, 100T, etc.), span, lifting height, and operational environment are defined.
Customization needs are assessed, such as control modes (pendant, wireless, cabin) and special features (e.g., anti-collision, overload protection).
Preliminary Design:
Structural engineers and crane designers create the crane's initial design, including the main beam, end carriage, lifting system, trolley system, travel mechanism, and other components.
Calculation and Simulation:
Load calculations are performed to ensure the crane can handle the specified capacity.
Finite element analysis (FEA) may be used to simulate stresses and deflections in the structure to ensure safety and stability.
Detailed Design:
After approval, detailed drawings for each part are made, including the main girder, end carriage, hoist system, motors, control systems, and safety features.
2. Material Procurement
Raw Material Selection:
High-quality materials like steel, alloyed steel, forged steel, and electrical components are sourced according to specifications.
Materials are inspected for quality certification and compliance with industry standards (e.g., ISO, CE).
Component Sourcing:
Standard components such as motors, hoists, control panels, limit switches, and safety devices are sourced from reliable suppliers.
3. Fabrication of Components
Main Girder:
Cutting and welding of steel plates to form the bridge girder.
The girder is assembled by welding or bolting sections, ensuring it meets the required strength and precision.
End Carriage Assembly:
The end carriage is fabricated and assembled to hold the crane on the runway rails.
Wheel assemblies are installed to ensure smooth travel along the rails.
Hoist and Trolley System:
The hoist unit (electric or manual) is assembled, including the drum, wire rope, hook, and motor.
The trolley system is built to transport the hoist across the bridge, including trolley wheels and drive mechanisms.
Crane Traveling Mechanism:
The crane wheels are mounted on the end carriages, ensuring smooth horizontal movement.
The drive system is installed to control travel speed.
4. Assembly of Crane
Main Beam Installation:
The assembled main girder is lifted and positioned onto the end carriages.
The girder is aligned to ensure structural integrity.
Trolley and Hoist Installation:
The trolley system is mounted onto the main girder, and the hoist is mounted to the trolley.
The load chain or wire rope is installed and tested for smooth operation.
Travel Mechanism Setup:
The crane wheels are fitted, and the drive mechanism is connected to the control system for horizontal movement.
5. Electrical and Control System Installation
Wiring and Control Panel:
The control panel is installed and wired to manage all crane movements (hoisting, trolley, crane travel).
Limit switches, emergency stop buttons, and safety alarms are integrated into the control system.
Motor and Gear Installation:
Motors for hoisting, traveling, and the trolley are installed and connected to their respective gear systems.
Testing of Control Systems:
Control systems are checked to ensure proper integration of pendant control, wireless remote, or cabin control options.
6. Testing and Quality Control
Load Testing:
The crane undergoes static load testing (to check stability) and dynamic load testing (to check operational performance under actual working conditions).
Overload protection and limit switches are tested to ensure they function correctly.
Safety System Testing:
The sound and light alarms, limit switches, emergency stop buttons, and safety devices are all tested for functionality.
Movement Testing:
All movements-hoisting, trolley movement, bridge travel, and sway control-are tested for smooth operation and precision.
Electrical Testing:
All electrical components are tested for proper wiring, grounding, and communication between systems.
Documentation and Certification:
The crane is inspected according to international safety standards and undergoes certification by relevant authorities (e.g., CE, ISO).
Test certificates for motors, cranes, and load testing are prepared.
7. Final Inspection and Painting
Visual Inspection:
A thorough inspection is carried out to ensure that the crane meets design specifications and safety requirements.
Painting:
The crane is painted with high-quality anti-corrosion coatings to protect it from environmental conditions.
Marking and Labeling:
Safety labels, warnings, and capacity markings are applied to the crane for proper identification.
8. Delivery and Installation
Shipping:
The crane is carefully disassembled into transportable parts (if needed) and shipped to the customer's location.
Installation:
The crane is installed on-site, and all connections (power, mechanical, control) are made.
Final Commissioning:
The crane is commissioned by running it through a series of operational tests to ensure it works properly.
Operator training is conducted, if necessary, for safe and efficient use.
9. Post-Installation Support
Customer Training:
Operator training on how to use the crane safely and effectively.
Maintenance Schedule:
Providing a maintenance plan for the crane's continued operation, including regular inspections, lubrication, and testing.
After-Sales Support:
Offering spare parts, troubleshooting, and repair services.
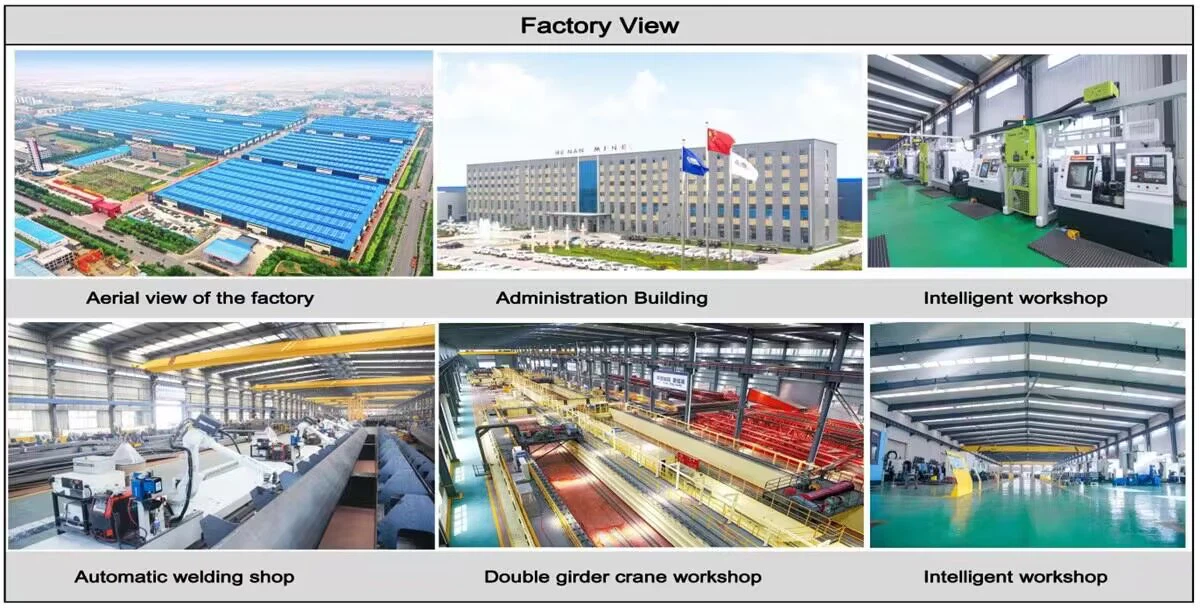
Workshop view:
The company has installed an intelligent equipment management platform, and has installed 310 sets (sets) of handling and welding robots. After the completion of the plan, there will be more than 500 sets (sets), and the equipment networking rate will reach 95%. 32 welding lines have been put into use, 50 are planned to be installed, and the automation rate of the entire product line has reached 85%.


Hot Tags: explosion proof european overhead crane, China explosion proof european overhead crane manufacturers, suppliers, factory, Double Girder Overhead Crane, Double Girder Overhead Travelling Crane
You Might Also Like


Send Inquiry