







European Explosion-proof Double-beam Crane
Products Description
Key Features of European Explosion-Proof Double-Beam Cranes:
Double-Girder Design
Provides higher lifting capacity (typically 5 tons to several hundred tons) and better stability compared to single-girder cranes.
Allows for longer spans and heavier-duty applications.
Explosion-Proof Components
Motors & Electrical Systems: Certified for Zone 1, Zone 2 (gas) or Zone 21, Zone 22 (dust) under ATEX or IECEx standards.
Control Systems: Explosion-proof pendant control or radio remote control.
Wiring & Junction Boxes: Sealed to prevent sparks.
Brakes & Limit Switches: Designed to avoid friction-induced sparks.
Safety & Compliance
Meets ATEX 2014/34/EU (for EU) or IECEx (international) standards.
Corrosion-resistant coatings for harsh environments (e.g., chemical plants, oil refineries).
Overload protection and emergency stop systems.
Comparison with Standard Cranes
| Feature | Explosion-Proof Double-Beam Crane | Standard Overhead Crane |
|---|---|---|
| Safety Certification | ATEX/IECEx compliant | Not rated for hazardous zones |
| Electrical Components | Spark-proof motors, sealed wiring | Standard motors & controls |
| Load Capacity | Up to 500+ tons (double-girder) | Typically ≤ 100 tons |
| Environmental Resistance | Corrosion/dust-proof construction | Basic protection |
| Cost | Higher initial investment | Lower cost |

Pictures & Components
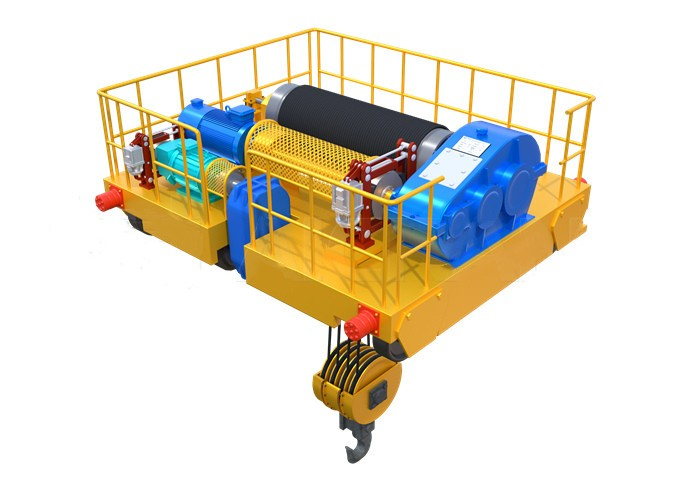
A European explosion-proof double-beam crane consists of several critical components, all designed to meet stringent safety standards (such as ATEX and IECEx) for operation in hazardous environments. Below is a detailed breakdown of its key components:
1. Main Structural Components
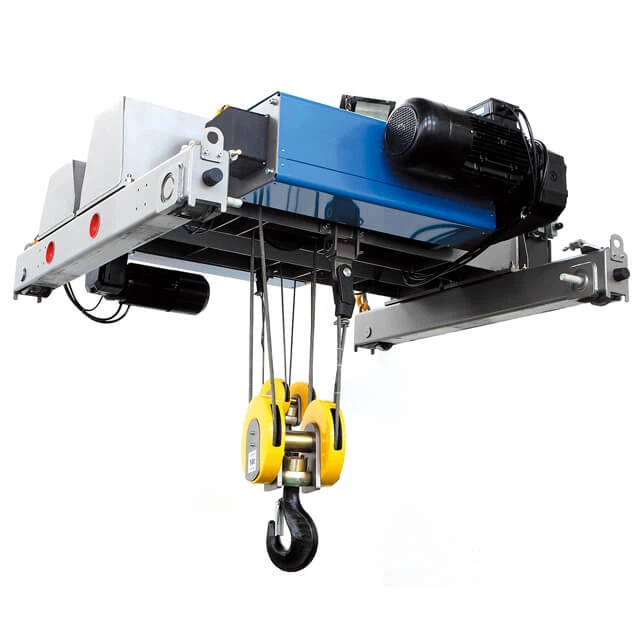
a) Double Beam (Box Girder or Truss Structure)
Made of high-strength steel for rigidity and load-bearing capacity.
Designed to prevent spark generation from friction or impact.
Often coated with anti-corrosion materials for harsh environments.
 |
 |
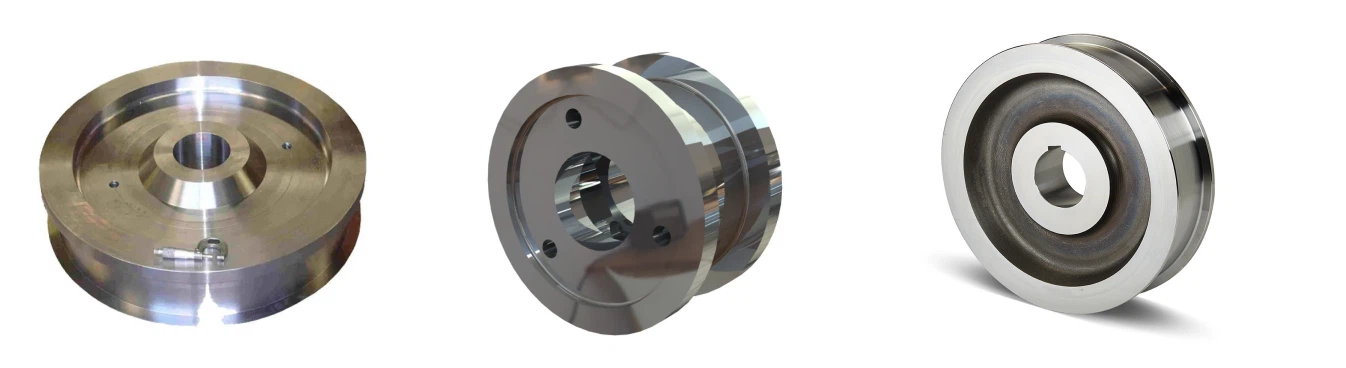
b) End Carriages & Wheels
Equipped with explosion-proof bearings and non-sparking wheel materials (e.g., bronze or special alloys).
May include flame-proof brakes for controlled stopping.
c) Runway Beam & Rails
Supports crane movement along the span.
Made of hardened steel with secure fastening to prevent misalignment.
 |
 |
2. Explosion-Proof Hoisting Mechanism
a) Explosion-Proof Hoist (Electric or Hydraulic)
Certified for ATEX Zone 1/21 (high-risk) or Zone 2/22 (medium-risk).
Options:
Wire rope hoist (higher lifting capacity, e.g., 5–100+ tons).
Chain hoist (compact, ideal for lower capacities).
Features spark-resistant gearboxes and encapsulated motors.
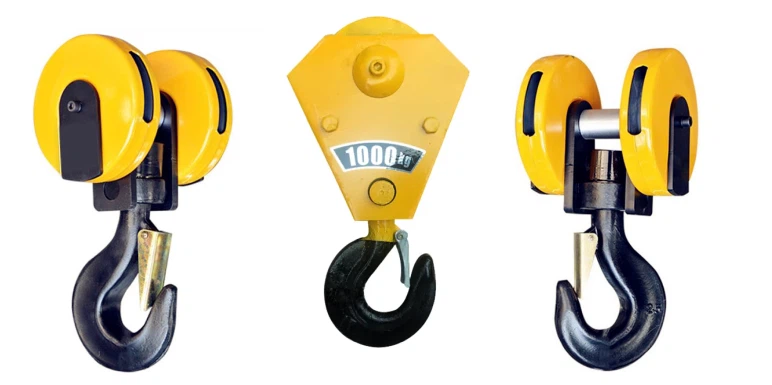
b) Hook Block & Load Sheave
Made of non-sparking materials (e.g., stainless steel or phosphor bronze).
Equipped with anti-sway technology for precise load handling.
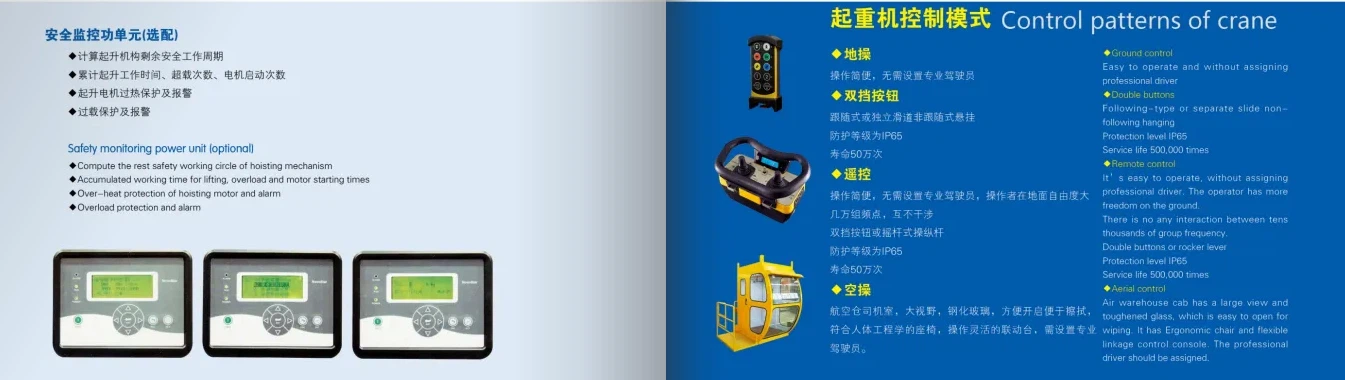
3. Electrical & Control Systems
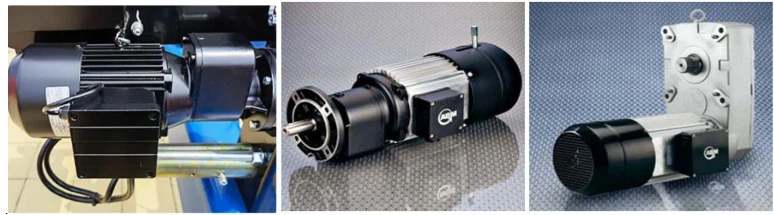
a) Explosion-Proof Motor & Gearbox
ATEX-certified motors (e.g., Ex d, Ex e, or Ex de rated).
Thermal protection to prevent overheating.
b) Explosion-Proof Control Panel & Wiring
Sealed enclosures (IP66 or higher) to prevent gas/dust ingress.
Intrinsically safe circuits to limit electrical energy below ignition levels.
c) Operator Controls
Explosion-proof pendant control (wired) or ATEX-certified radio remote control.
Emergency stop button with fail-safe braking.
d) Limit Switches & Sensors
Spark-proof limit switches for upper/lower travel limits.
Overload protection system to prevent crane overloading.

4. Safety & Auxiliary Components
a) Explosion-Proof Lighting
LED work lights with Ex d or Ex e certification for hazardous zones.
b) Cable Reels & Energy Supply
Trailing cable systems with flame-resistant insulation.
Slip ring assemblies (for rotating connections) with spark-proof design.
c) Anti-Collision & Monitoring Systems
Laser or ultrasonic sensors for collision avoidance.
Condition monitoring (temperature, vibration sensors) for predictive maintenance.
.

5. Compliance & Certification
Each component must meet:
ATEX 2014/34/EU (EU Directive for explosive atmospheres).
EN 15011 (European standard for overhead cranes).
IECEx (International Explosion-Proof Certification).
ISO 13849-1 (Safety of machinery).

Typical Hazardous Area Classifications
| Zone | Risk Level | Application Example |
|---|---|---|
| Zone 1 | Explosive gas mixture likely | Oil refineries |
| Zone 2 | Explosive gas mixture unlikely | Fuel storage |
| Zone 21 | Combustible dust likely | Grain silos |
| Zone 22 | Combustible dust unlikely | Coal handling |
SKETCH

Main technical

Advantages
European explosion-proof double-beam cranes are engineered for safety, durability, and efficiency in hazardous environments. Here are their key advantages:
1. Enhanced Safety in Explosive Atmospheres
ATEX/IECEx-certified components prevent sparks, arcs, and overheating.
Flame-proof enclosures on motors, controls, and wiring eliminate ignition risks.
Fail-safe braking & overload protection ensure controlled operations.
2. High Load Capacity & Stability
Double-girder design supports 5 to 500+ tons, ideal for heavy-duty lifting.
Reduced deflection compared to single-girder cranes, ensuring precise load handling.
3. Durability in Harsh Conditions
Corrosion-resistant coatings (epoxy, stainless steel) for chemical plants, offshore rigs, and mining.
Sealed bearings & dust-proof mechanisms for abrasive or dusty environments.
4. Customizable for Hazardous Zones
Configurable for Zone 1/2 (gases) or Zone 21/22 (dust) per ATEX standards.
Options include explosion-proof hoists, radio remote controls, and anti-static trolleys.
5. Energy Efficiency & Smooth Operation
Variable frequency drives (VFDs) reduce power consumption and enable soft starts/stops.
Low-maintenance components (sealed gears, lubricated-for-life bearings).
6. Compliance with Strict European Standards
Meets ATEX 2014/34/EU, EN 15011, IECEx, and ISO 13849 for safety and reliability.
Application:
1. Oil & Gas Industry
Refineries, drilling platforms, petrochemical plants – Handling pipes, valves, and machinery in explosive gas zones (Zone 1/2).
2. Chemical & Pharmaceutical Manufacturing
Moving flammable solvents, powders, or reactive chemicals (Zone 1/21).
3. Grain & Food Processing
Flour mills, sugar plants, grain silos – Preventing dust explosions (Zone 21/22).
4. Mining & Underground Facilities
Lifting equipment in methane-rich or coal dust environments.
5. Paint & Coating Facilities
Safe handling of flammable paints, solvents, and aerosols (Zone 1).
6. Aerospace & Defense
Transporting fuel tanks, explosives, or munitions in controlled environments.
7. Waste Treatment & Biofuel Plants
Managing biogas, hydrogen, or combustible waste materials.
Crane production procedure
The production procedure for an Electric Hoist Double Beam Bridge Crane involves several key stages, from design and material procurement to assembly and testing. Below is a general step-by-step outline of the manufacturing process:
1. Design & Engineering
Customer Requirements Analysis: Determine load capacity, span, lifting height, duty cycle (FEM/ISO classification), and environmental conditions.
Structural Design:
Design the double girder bridge (main beams, end carriages) using CAD software (e.g., AutoCAD, SolidWorks).
Calculate stresses, deflection, and fatigue life per standards (ISO, DIN, FEM, or ASME).
Electrical & Mechanical Design:
Select hoist type (wire rope/electric chain hoist), motor power, control system, and safety devices (limit switches, overload protection).
Approval: Finalize drawings and get client/regulatory approval.
2. Material Procurement
Main Beams: Steel plates (Q235B, Q345B) or prefabricated I-beams.
End Carriages: Fabricated from steel sections (channels, angles) or welded plates.
Electrical Components: Hoist, motors, gearboxes, wheels, brakes, cables, and pendant/radio remote control.
Other Components: Rails, buffers, hooks, and safety devices.
3. Fabrication of Main Components
A. Double Girder Fabrication
Cutting: Steel plates are cut to size (laser/plasma/oxyfuel cutting).
Welding:
Fabricate box-type or I-section girders via submerged arc welding (SAW) or MIG/MAG welding.
Stress-relieving (heat treatment) to prevent distortion.
Machining: Drill holes for connections and surface machining (if required).
B. End Carriage Assembly
Welded Construction: Fabricate end carriages with wheels, buffers, and drive mechanisms.
Wheel Installation: Mount forged steel wheels with bearings for bridge movement.
C. Hoist Trolley Assembly
Frame Construction: Build trolley frame to mount the electric hoist.
Drive Mechanism: Install motors, gearboxes, and wheels for trolley travel along the girders.
4. Surface Treatment & Painting
Blasting: Shot-blasting to remove rust and improve paint adhesion.
Priming/Painting: Apply anti-corrosion primer and topcoat (usually epoxy or polyurethane).
Curing: Bake or air-dry painted components.
5. Electrical System Installation
Wiring: Install power supply systems (festoon/cable reels), control panels, and sensors.
Hoist Integration: Mount the electric hoist (wire rope or chain) onto the trolley.
Safety Devices: Install limit switches, overload protection, and emergency stop.
6. Assembly & Testing
A. Bridge Assembly
Girder-End Carriage Joining: Bolt or weld girders to end carriages.
Alignment Check: Ensure parallel girders and proper wheel alignment.
B. Functional Tests
No-Load Test: Run crane without load to check movement (hoisting, trolley, bridge travel).
Load Test:
Static Test: 125% of rated load (held for 10+ minutes to check deformation).
Dynamic Test: 110% of rated load to verify performance under motion.
Safety Checks: Verify brakes, limit switches, and emergency stops.
7. Quality Inspection & Certification
Dimensional Checks: Verify span, lift height, and alignment.
NDT Testing: Ultrasonic/X-ray welding inspections (if required).
Certification: Issue compliance certificates (CE, ISO, OSHA, or local standards).
8. Disassembly & Packaging
Modular Dismantling: Break down into transportable sections (girders, end carriages, hoist).
Packaging: Protect components with waterproof wrapping and secure for shipping.
9. Installation & Commissioning (On-Site)
Reassembly: Erect runway rails, assemble bridge, and mount hoist/trolley.
Final Testing: Perform on-site load tests and operator training.
10. Documentation & Delivery
Provide manuals (operation, maintenance), test reports, and warranty documents.
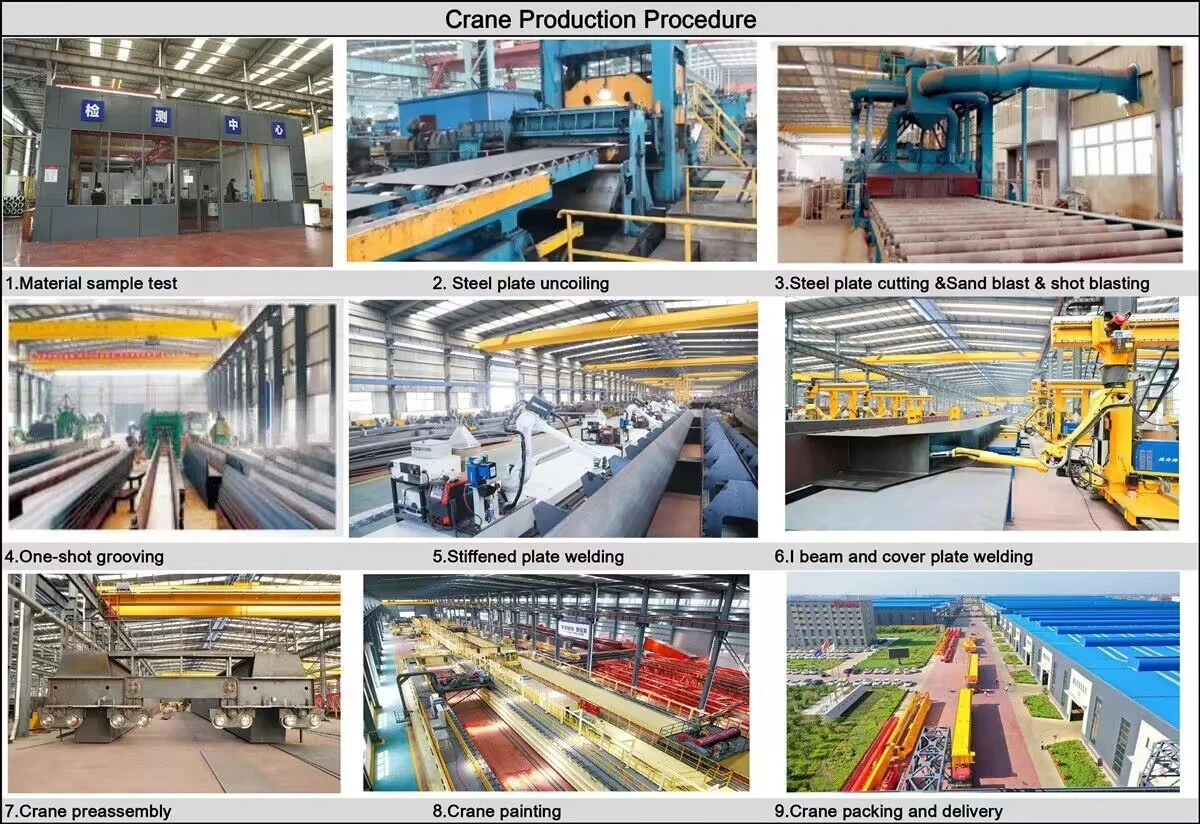
Workshop view:
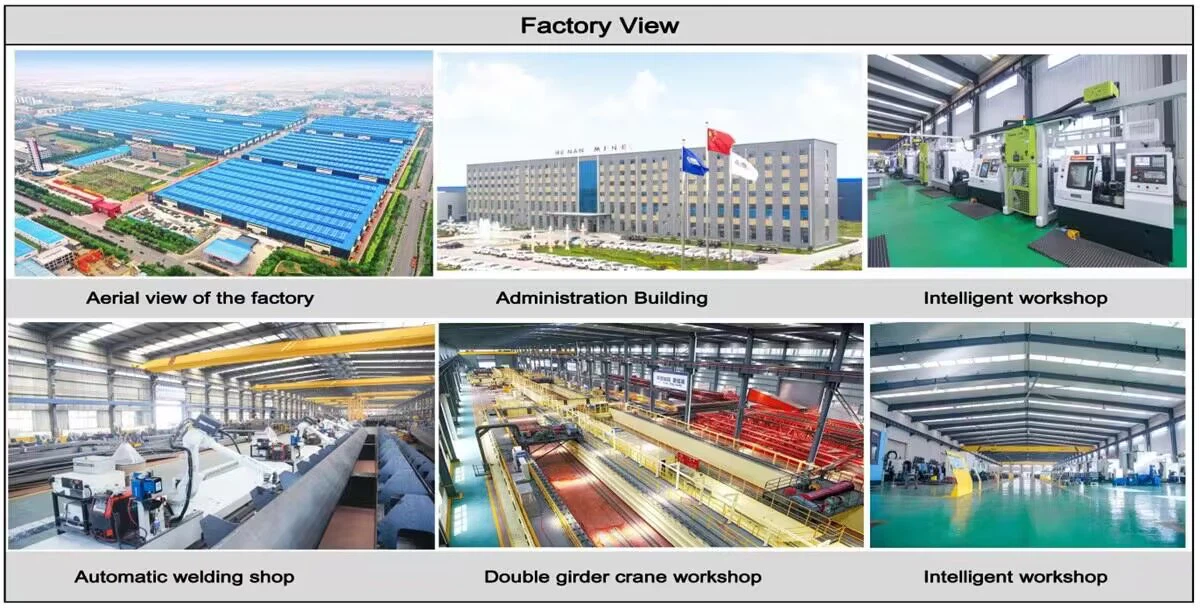
The company has installed an intelligent equipment management platform, and has installed 310 sets (sets) of handling and welding robots. After the completion of the plan, there will be more than 500 sets (sets), and the equipment networking rate will reach 95%. 32 welding lines have been put into use, 50 are planned to be installed, and the automation rate of the entire product line has reached 85%.


Hot Tags: european explosion-proof double-beam crane, China european explosion-proof double-beam crane manufacturers, suppliers, factory, Double Girder Overhead Crane, Double Girder Overhead Travelling Crane
You Might Also Like


Send Inquiry