





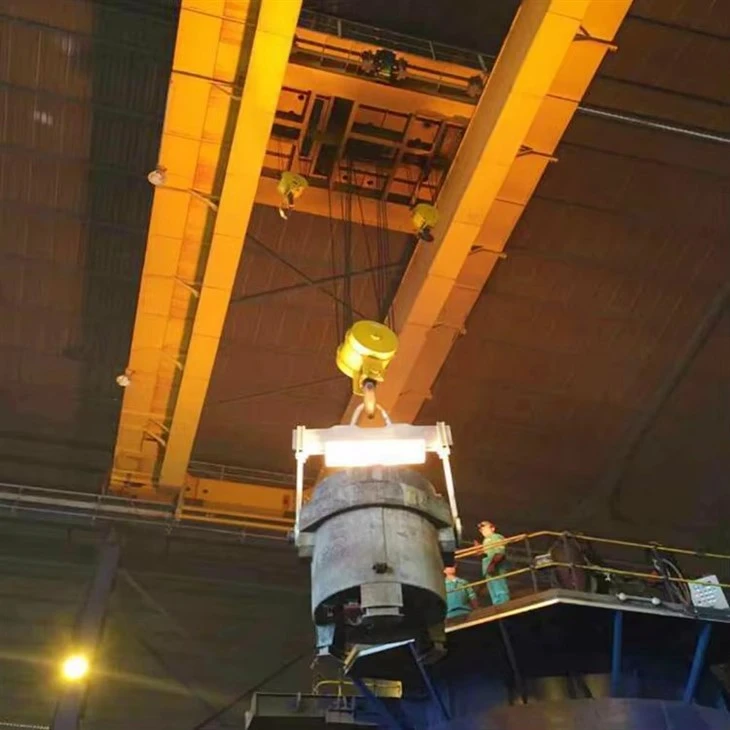

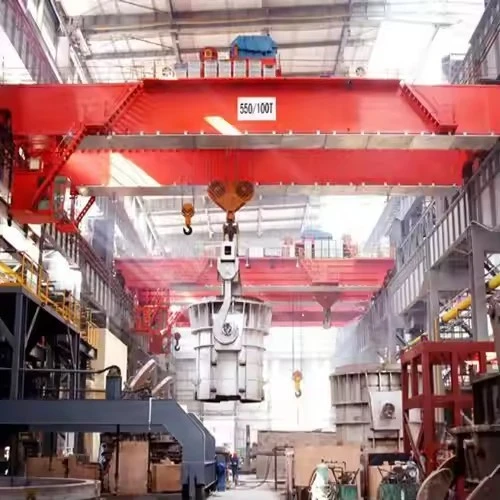
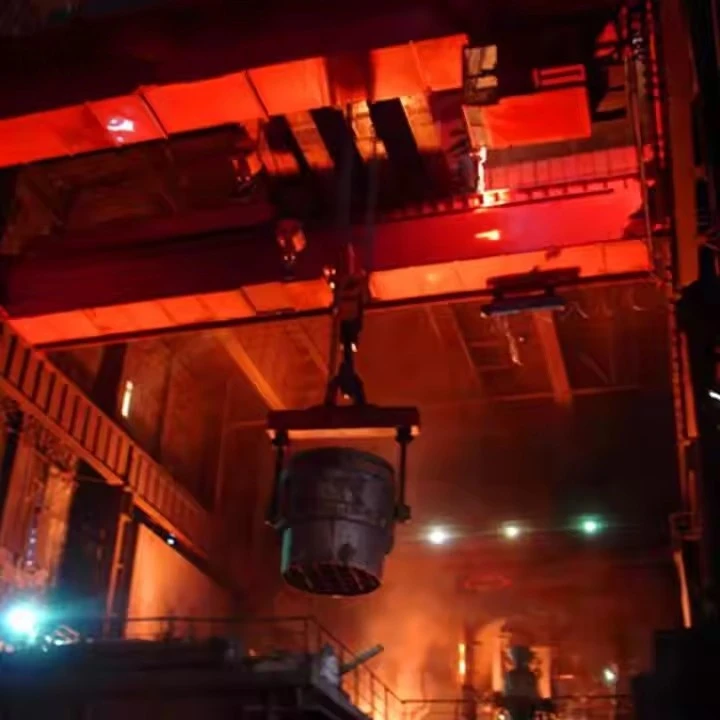
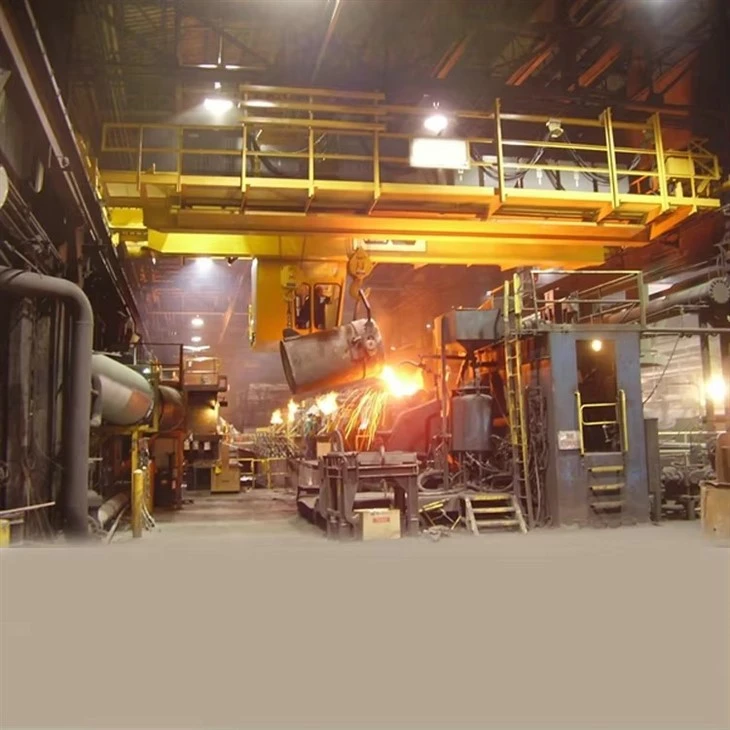
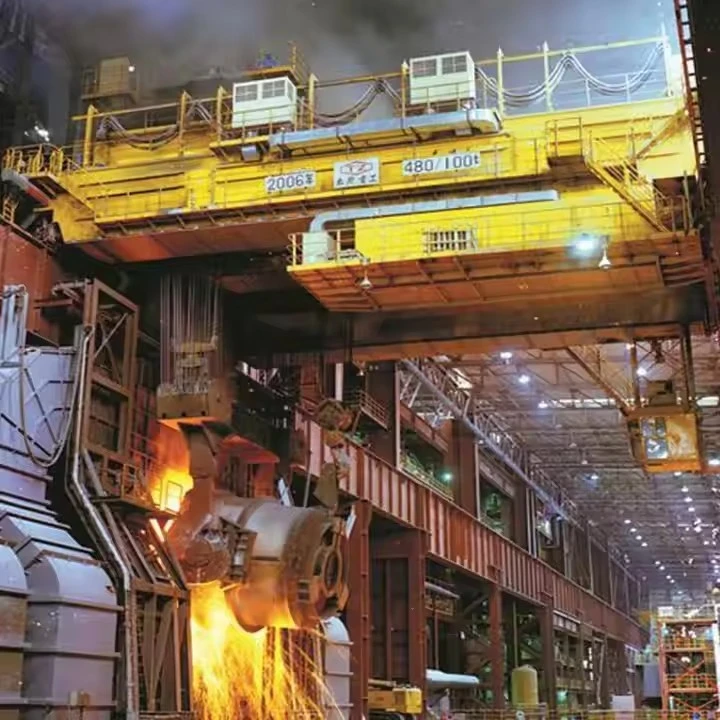
QDY Metallurgic Double Girder Casting Overhead Crane
Products Description
Why Choose a QDY Crane?
You select a QDY Metallurgic Double Girder Casting Crane over a standard overhead crane when:
The Load is Hazardous: You are handling molten metal.
Safety is Paramount: The consequences of a failure are catastrophic. The redundant systems are non-negotiable.
Precision is Required: The process demands exact pouring control to ensure product quality and operator safety.
The Environment is Extreme: The crane is exposed to intense heat, sparks, and dust.
Uptime is Critical: The crane is an integral part of a continuous, high-value production process where downtime costs thousands of dollars per minute.
Comparison vs. Standard Double Girder Cranes
| Feature | QDY Metallurgical Crane | Standard Double Girder Crane |
|---|---|---|
| Primary Use | Handling molten metal ladles | General material handling |
| Safety Features | Redundant systems: dual brakes, dual motors, heat shields | Standard single brakes, no special heat protection |
| Lifting Attachment | Specialized ladle lifting beam or C-hook | Standard hook |
| Control Precision | Extremely high (for pouring), with VFDs on all motions | Can be basic or precise, depending on option |
| Environmental Protection | High: Heat, spark, and dust resistance | Minimal |
| Cost | Significantly Higher | Lower |
Core Components:Bearing, Gearbox, Motor, Pump
Place of Origin:Henan, China
Warranty:1 Year
Weight (KG):2000 kg
Video outgoing-inspection:Provided
Machinery Test Report:Provided
Design:Double beam
Effectiveness:high efficiency
Operating speed:High speed operation
Stability:Anti-swing function
Color:Optional
Power Source:110V/220V/230V/380V/440V,customized
Span:7.5-31.5m

Pictures & Components
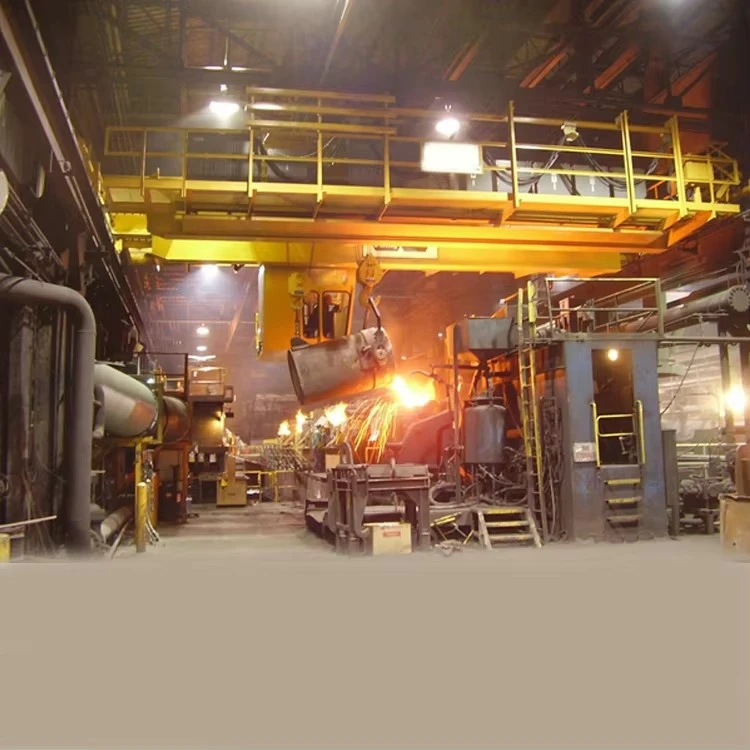
This crane is a complex system of integrated parts designed for maximum safety and reliability in the extreme environment of molten metal handling. The components can be categorized into several critical systems.
1. Structural System (The Heavy-Duty Frame)
This system is built to withstand immense weight, heat, and thermal shock.
Main Bridge Girders (Double Girder): Two extremely robust, fabricated steel box girders that form the primary load-bearing horizontal beam. They are made from high-tensile steel plates and are designed to resist bending (deflection) under the full ladle load and thermal expansion.
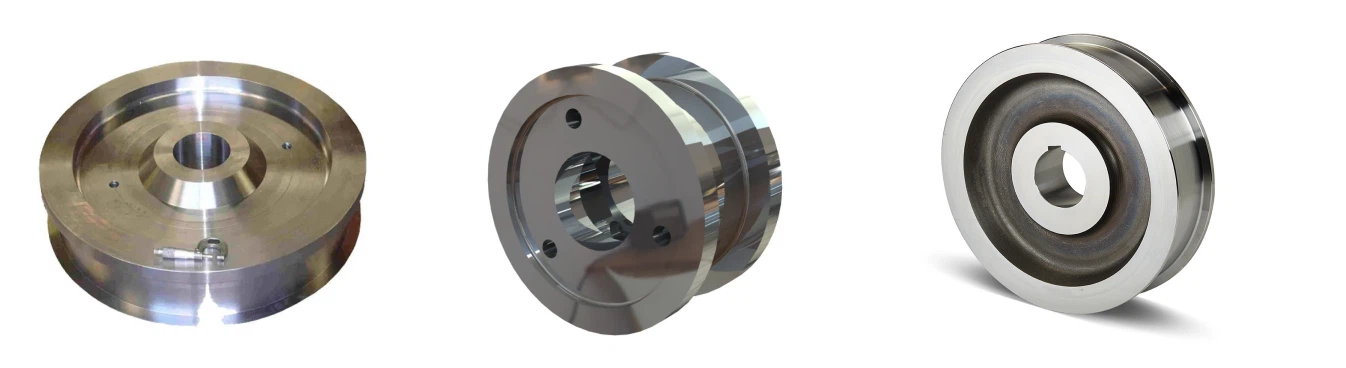
End Trucks & Travel Bogies: The assemblies at each end of the bridge that house the components for moving the entire crane.
Travel Wheels: Large-diameter, forged or alloy steel wheels that run on the runway rails. They are often equipped with double-rims to prevent derailment from track misalignment.
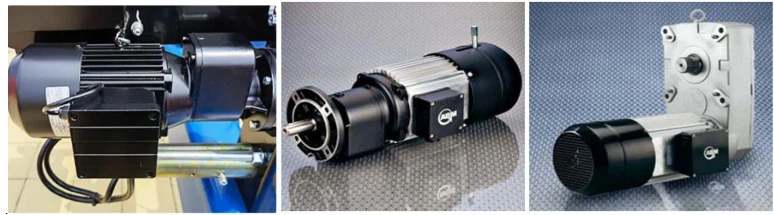
Drive Motors: Powerful, well-sealed electric motors that power the travel wheels.
Bevel Gear Reducers: Provide the torque needed to move the massive crane along the runway.
Runway System: The fixed track the crane moves on. For a QDY crane, this is a heavily reinforced structure, often using strong steel rails like QU100 or QU120.
 |
 |
2. Hoisting and Tilting System (The Core Machinery)
This is the heart of the casting crane, designed with massive redundancy.
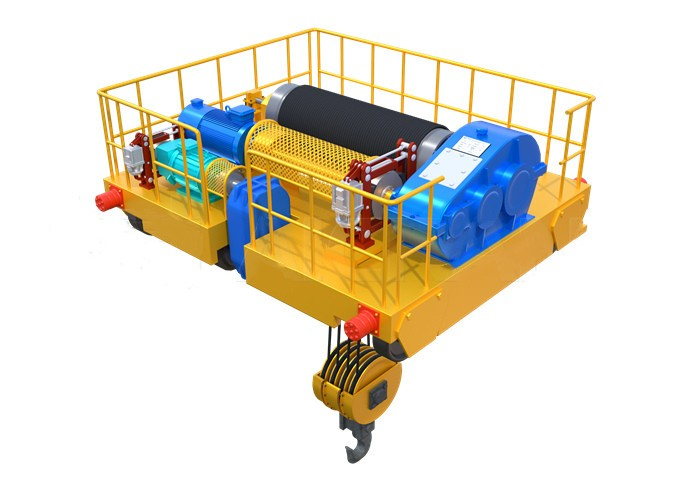
Main Hoist Assembly: The primary system for lifting the full ladle.
Hoist Motor(s): Often features dual motors (twin-drive) for redundancy. If one motor fails, the other can safely lower the load.
Geared Reducer: A heavy-duty, high-torque gearbox that translates the motor's power into lifting force.
Drum: The large steel cylinder around which the wire rope is wound.
Wire Rope & Sheaves: High-grade, heat-resistant steel wire rope that runs over specially designed pulleys (sheaves). The rope is often equipped with stainless steel guards for spark and heat protection.
 |
 |
Auxiliary Hoist / Tilting Mechanism: The system for controlling the pour.
This is typically a second, independent hoist unit or a dedicated hydraulic system that connects to the ladle's tilting mechanism.
It allows the operator to precisely control the angle of the ladle for pouring, with very fine, gradual movement to prevent splashing.
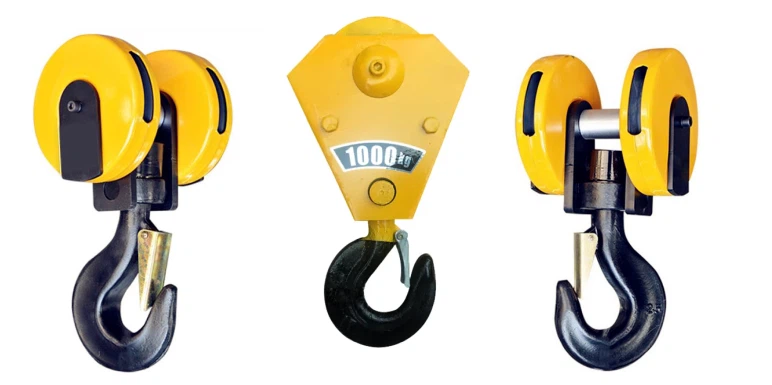
Ladle Lifting Beam (or C-Hook): A specialized, water-cooled or heat-shielded attachment that connects to the trunnions of the molten metal ladle. It is not a standard hook.
3. Trolley System (The Movement on the Bridge)
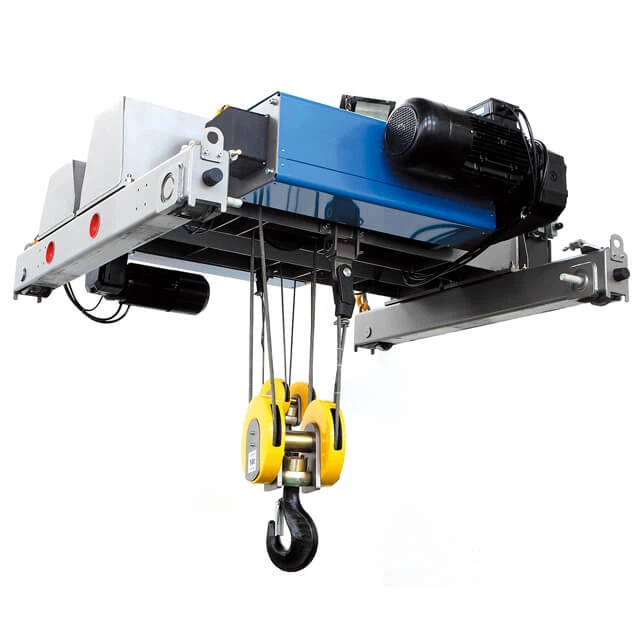
Trolley Frame: A heavy steel frame that carries both the main and auxiliary hoists and runs on rails mounted on top of the two main girders.
Trolley Drive: Consists of a motor, brake, and reducer that power the wheels to move the trolley (and the ladle) across the width of the crane bay.
4. Power and Electrical System (The Nervous System)
Designed for reliability and protection in a harsh environment.
Insulated / Air-Conditioned Control Panel: The electrical cabinet is a sealed, insulated unit, often with its own cooling system, to protect sensitive components (PLCs, contactors, VFDs) from radiant heat and conductive dust.
Variable Frequency Drives (VFDs): Installed for all motions (main hoist, auxiliary hoist, trolley, bridge travel). They provide extremely smooth, controlled acceleration and deceleration, which is critical for preventing ladle sway and ensuring precise pouring.

Conductor Bar System (Enclosed Track): A fully enclosed, robust power delivery system that runs the length of the runway. It is far more reliable and resistant to dust and splashes than a festoon system.
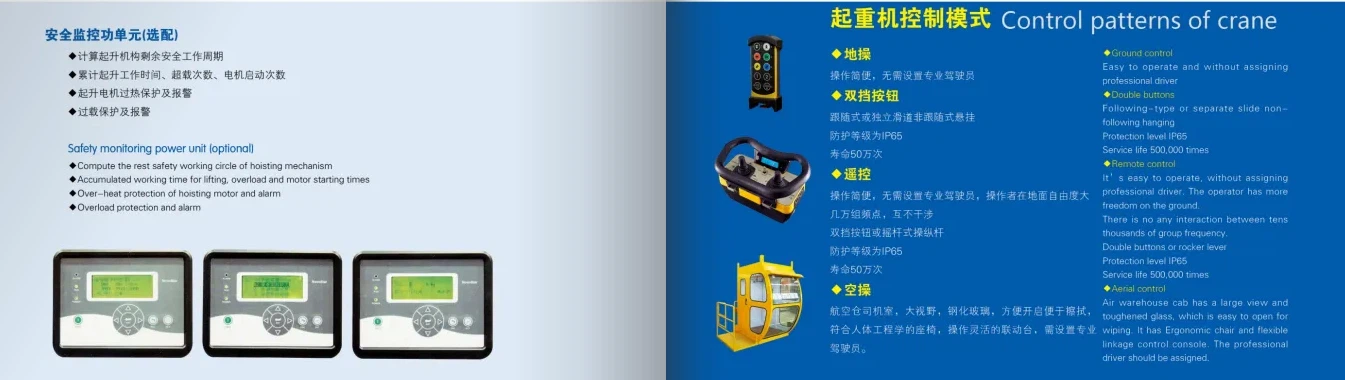
Operator's Cabin: Heavily insulated and air-conditioned with heat-reflective glass. It can be mounted on the crane bridge or, more commonly, operated via Radio Remote Control to keep the operator at a safe distance.
5. Safety and Protection Systems (The Fail-Safes)
This is what truly defines a QDY casting crane. Redundancy is key.
Dual Braking Systems (Main Hoist):
Service Brake: A primary, electrically released disc brake.
Safety Brake: A secondary, mechanically applied brake (often on the low-speed side of the reducer) that acts as a backup. Both are fail-safe (spring-applied, electrically released).
Overload Limiter: An electronic sensor that prevents the crane from lifting a load beyond its rated capacity. It is a critical safety device.

Anti-Sway System: An advanced software system that works with the VFDs to automatically compensate for and prevent the pendulum motion of the ladle during travel.
Ladle Weighing System: A built-in scale that provides real-time weight measurement of the molten metal to the operator.
Heat Shields and Guards: Protective plates installed on the girders, end trucks, and electrical panels to deflect radiant heat from the ladle below.
Anemometer: A wind speed sensor that can alert the operator or automatically slow/stop crane travel if wind speeds become dangerous for the large ladle.
Sketch

Main technical

Advantages
The advantages of this crane are defined by its unparalleled safety features, robustness, and precision in extreme conditions.
1. Ultimate Safety and Redundancy
Fail-Safe Design: This is the core advantage. The system is designed with the philosophy that any single point of failure should not lead to a catastrophe. Key features include:
Dual Hoist Motors (Twin-Drive): If one motor fails, the other can safely lower the ladle.
Dual Braking Systems: Includes a primary service brake and a secondary, mechanically applied safety brake on the hoist. Both are typically spring-set, meaning they engage automatically if power is lost.
Overload Limiter: Prevents the crane from lifting beyond its rated capacity, a critical feature given the immense value and danger of the load.
Ladle Weighing System: Provides real-time weight data to the operator, crucial for process control and ensuring the load does not exceed safe limits.
2. Exceptional Reliability and Uptime
Robust Construction: Built with heavy-duty, fabricated steel girders and high-quality mechanical components to withstand continuous use in a 24/7 production environment like a steel mill. Minimizing downtime is a primary economic driver.
Protected Components: Electrical panels are insulated and often air-conditioned to protect sensitive PLCs, VFDs, and wiring from the intense radiant heat, which significantly reduces electrical failures.
3. Superior Precision and Control
Variable Frequency Drives (VFDs): Standard on all motions (hoist, trolley, bridge). VFDs allow for incredibly smooth acceleration and deceleration, enabling:
Anti-Sway Control: Automatically prevents the ladle from swinging during transport, a major safety hazard.
Precise Pouring: The auxiliary hoist/tilting mechanism allows for fine, gradual control to tip the ladle, ensuring an accurate pour without splashing molten metal.
4. Built for Extreme Environments
Heat Resistance: Equipped with heat shields on the girders and end trucks, high-temperature paint, and often water-cooled components (like the lifting beam) to protect the crane from thermal damage.
Spark and Dust Protection: Features like stainless steel wire rope guards and sealed electrical components prevent damage from sparks and conductive dust, which are prevalent in metallurgical plants.
5. Enhanced Operator Safety and Ergonomics
Radio Remote Control: Allows operators to control the crane from a safe distance, with an optimal view of the ladle and pouring process, away from heat and potential splash zones.
Insulated Cabin: If cabin-operated, it is fully equipped with air conditioning and heat-reflective glass to protect the operator.
Application:
The application of this crane is highly specific and critical to the primary production process in metal smelting and foundries.
1. Primary Application: Molten Metal Ladle Handling
The core function is to transport a ladle filled with molten metal and pour it into another vessel or mold. This includes:
Charging Furnaces: Transporting molten iron from a mixer or blast furnace to a Basic Oxygen Furnace (BOF) or Electric Arc Furnace (EAF).
Example: Moving a ladle of molten iron from the blast furnace to the steelmaking converter.
Pouring and Casting:
Continuous Casting: Feeding molten steel from the ladle into the tundish and mold of a continuous casting machine.
Ingot Casting: Pouring molten metal into large molds to form ingots or slabs.
Foundry Pouring: In foundries, precisely pouring molten iron, steel, or other metals into sand molds or other mold types to create castings.
2. Specific Industry Workflows
Integrated Steel Mills:
Transport molten iron from the blast furnace to the steelmaking shop.
Handle ladles in the continuous casting bay.
Foundries (Ferrous and Non-Ferrous):
Lift pouring vessels (ladles, crucibles) from holding furnaces (e.g., cupola, induction furnace) and transport them to pouring stations to fill molds.
Non-Ferrous Smelters (Aluminum, Copper):
Handling large crucibles or ladles of molten aluminum or copper for alloying, transfer, or casting processes.
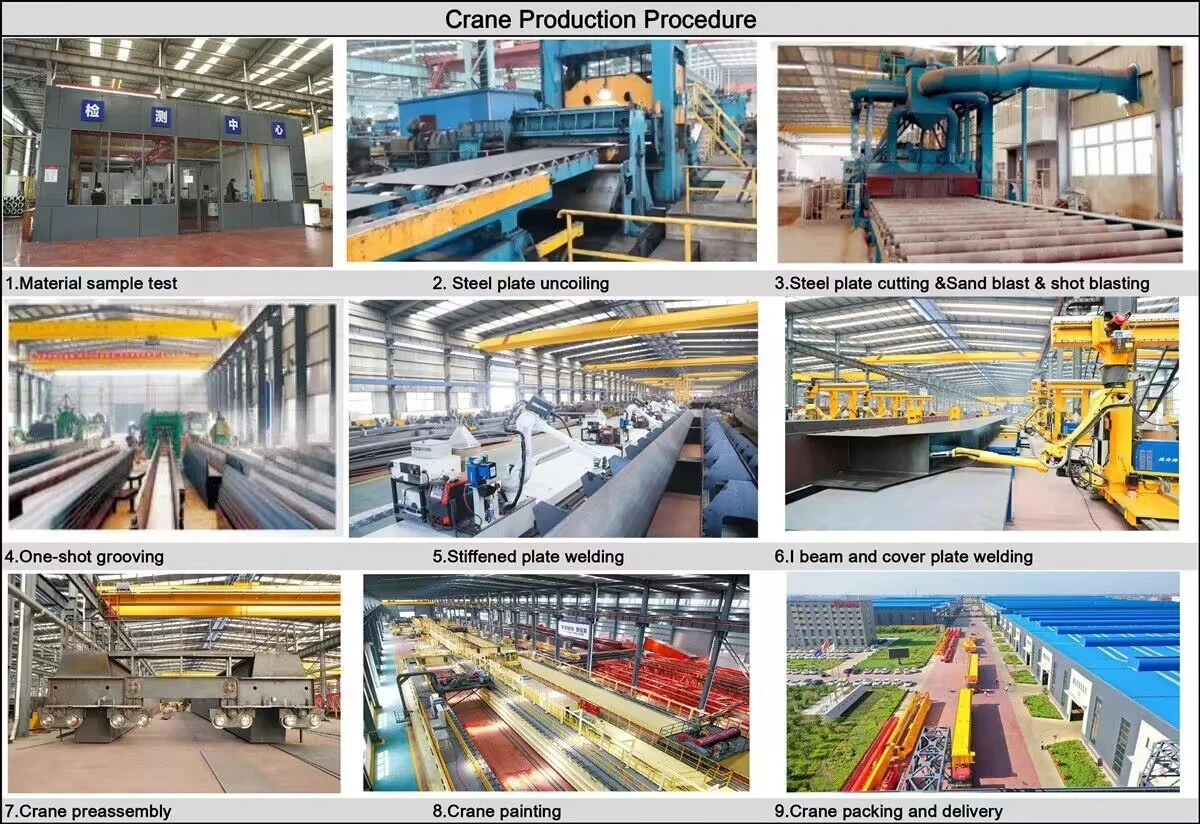
Crane production procedure
The manufacturing process of a QDY metallurgical casting bridge crane involves strict quality control and specialized engineering to ensure durability, heat resistance, and safety. Below is a step-by-step breakdown of the production procedure:
1. Design & Engineering
Load & Environment Analysis – Calculations for lifting capacity (5–500+ tons), span, and heat resistance.
CAD/3D Modeling – Structural design, stress simulations (FEA), and compliance with ISO, FEM, or GB standards.
Customization – Optional features (explosion-proofing, insulated hoists, automation) are integrated.
2. Material Selection & Preparation
Main Girders & End Carriages – High-strength steel (Q345B, Q460C) or heat-resistant alloy steel.
Wire Ropes & Hooks – Special heat-treated alloy steel (for molten metal handling).
Electrical Components – High-temperature-resistant cables, motors, and insulation materials.
3. Fabrication of Key Components
A. Bridge Girder Construction
Cutting & Welding – CNC plasma/laser cutting for precision; submerged arc welding (SAW) for high-strength joints.
Heat Treatment – Stress-relieving annealing to prevent deformation.
Machining – Drilling, milling, and surface grinding for assembly accuracy.
B. Hoist & Trolley Assembly
Hoist Drum & Gearbox – Machined for smooth operation; tested under 1.25x rated load.
Heat-Resistant Brakes – Dual-disc or electromagnetic brakes for fail-safe holding.
Ladle Hook & Safety Latch – Forged and ultrasonically tested for cracks.
C. End Trucks & Runway System
Wheel & Rail Machining – Hardened steel wheels for long wear life.
Drive Motors & Reducers – Equipped with anti-skid mechanisms for heavy loads.
4. Electrical & Control System Integration
Festoon/Conductor Bar System – For power supply along the runway.
Variable Frequency Drives (VFDs) – For smooth speed control and energy efficiency.
Safety Circuits – Overload sensors, limit switches, and emergency stop.
Operator Controls – Pendant, cabin, or remote/automated systems.
5. Surface Treatment & Corrosion Protection
Sandblasting (SA 2.5 Grade) – Removes rust and improves paint adhesion.
High-Temp Paint/Coating – Zinc-rich primer + heat-resistant topcoat (up to 800°C).
Critical Component Insulation – Ceramic fiber or refractory coatings on hooks and ropes.
6. Assembly & Testing
A. Pre-Assembly Checks
Dimensional inspection of girders, trolley, and end carriages.
Alignment of runway rails and crane tracks.
B. Load Testing (Per ISO 4310 / GB Standards)
No-Load Test – Checks motor, brake, and travel functions.
Static Load Test – 1.25x rated capacity for 10+ minutes.
Dynamic Load Test – 1.1x rated capacity with repeated movements.
Emergency Brake Test – Verifies fail-safe mechanisms.
C. Heat Resistance Validation (For Foundry Cranes)
Simulated high-temperature exposure (if required).
7. Packaging & Delivery
Disassembly (if needed) – For large cranes, components are shipped separately.
Anti-Corrosion Packaging – VCI film or desiccant for overseas transport.
Documentation – Manuals, test reports, and certifications (CE, ISO, GOST, etc.).
8. Installation & Commissioning (On-Site)
Runway alignment and crane reassembly.
Final load testing and operator training.
Workshop view:
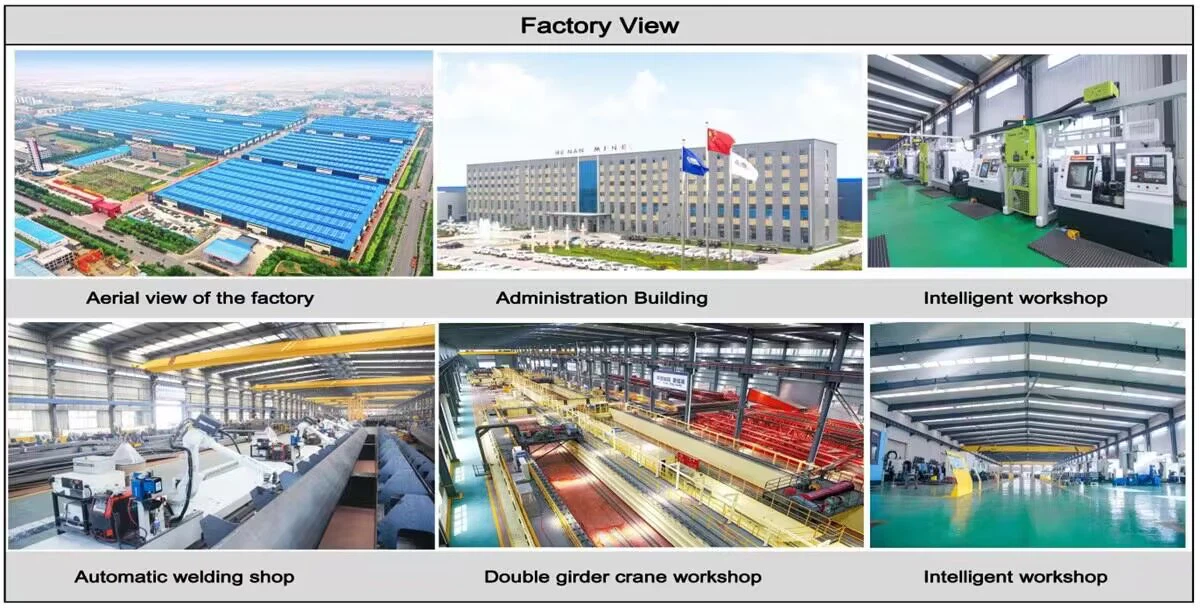
The company has installed an intelligent equipment management platform, and has installed 310 sets (sets) of handling and welding robots. After the completion of the plan, there will be more than 500 sets (sets), and the equipment networking rate will reach 95%. 32 welding lines have been put into use, 50 are planned to be installed, and the automation rate of the entire product line has reached 85%.


Hot Tags: qdy metallurgic double girder casting overhead crane, China qdy metallurgic double girder casting overhead crane manufacturers, suppliers, factory, Double Girder Overhead Travelling Crane, Double Girder Overhead Crane
You Might Also Like





Send Inquiry