






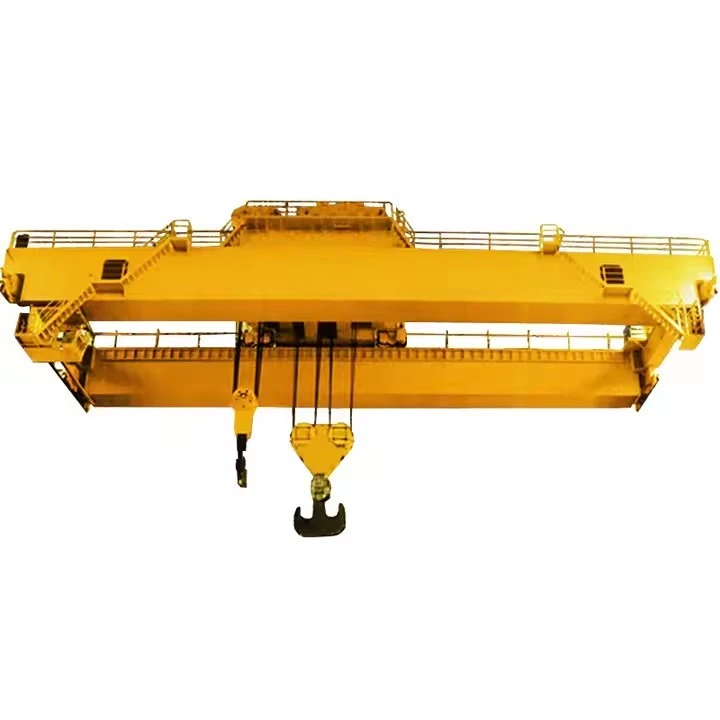


Ld Overhead Crane
Products Description
Choosing Between Manual & Automated
Consider these factors:
Budget (automated costs 2-3× more)
Production volume (high volume = automation)
Precision needs (automated offers ±1mm accuracy)
Labor availability (automated reduces staffing needs)
Types of Overhead Cranes
| Type | Description | Best For |
|---|---|---|
| Manual Overhead Crane | Operated via pendant/joystick | Workshops, maintenance |
| Semi-Automated Crane | Partial automation with some manual control | Mixed operations |
| Fully Automated Crane | PLC-controlled, no operator needed | High-volume production |
Core Components: Gearbox, Motor, Gear
Place of Origin: Henan, China
Warranty: 1 Year
Weight (KG): 10000 kg
Video outgoing-inspection: Provided
Machinery Test Report: Provided
Selling Units: Single item
Single package size: 600X300X300 cm
Single gross weight: 200.000 kg

Pictures & Components
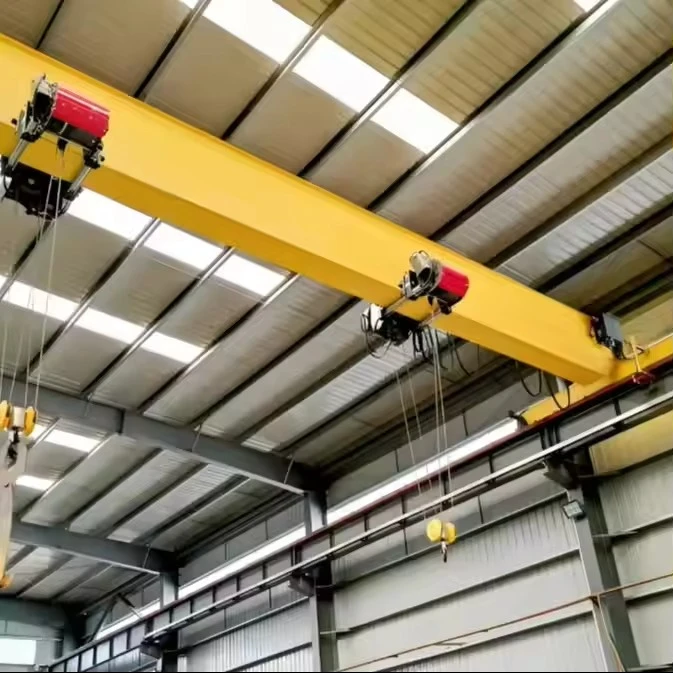
Overhead cranes (also called bridge cranes) consist of structural, mechanical, electrical, and control components that work together to lift and move heavy loads. Below is a detailed breakdown of their key parts, covering both manual and automated versions.
1. Structural Components
A. Bridge Girder
The main horizontal beam that spans the work area.
Types:
Single girder (lighter loads, cost-effective)
Double girder (heavy-duty, higher capacity)

B. Runway System
Supports the crane's movement along the length of the facility.
Types:
Top-running (rails mounted on runway beams)
Underhung (suspended from ceiling structures)
C. End Trucks
Wheeled assemblies at each end of the bridge that move along the runway.
Include drive motors, wheels, and brakes.
 |
 |
2. Lifting & Movement Components
A. Hoist Unit
The lifting mechanism (electric or manual).
Types:
Wire rope hoist (for heavy loads)
Chain hoist (compact, for lighter loads)
 |
 |
B. Trolley
Moves the hoist side-to-side along the bridge girder.
Can be manual push, motorized, or fully automated.
C. Hook Block & Load Attachment
Hook, grab, magnet, or vacuum lifter (depends on load type).
May include load sensors for weight monitoring.

3. Power & Control Systems
A. Manual Control (Pendant/Radio Remote)
Pendant station (hanging control) or wireless remote.
Basic up/down, left/right, forward/backward movements.

B. Automated Control (PLC & Drives)
Programmable Logic Controller (PLC) – Executes automated sequences.
Variable Frequency Drives (VFDs) – Smooth speed control.
Human-Machine Interface (HMI) – Touchscreen for programming.
C. Power Supply
Festoon system (cable management for moving power).
Busbar system (alternative for high-duty cycles).

4. Safety & Sensor Components
A. Limit Switches
Prevent over-travel of the bridge, trolley, and hoist.
B. Overload Protection
Load cells detect excess weight and stop operation.
.
C. Emergency Stop (E-Stop)
Instantly cuts power in emergencies.
D. Anti-Collision Systems (Automated Cranes)
Laser, ultrasonic, or infrared sensors prevent crashes.
E. Anti-Sway Technology (Automated Cranes)
Reduces load swinging during movement.

Additional Features in Automated Cranes
| Component | Function |
|---|---|
| Encoders | Precise position feedback |
| RFID/Barcode Readers | Automated load identification |
| IoT Sensors | Remote monitoring & predictive maintenance |
| Automated Guided Vehicle (AGV) Interface | Integration with robotic systems |

Sketch

Main technical

Advantages
1. Key Advantages of Overhead Cranes
A. For Manual Overhead Cranes:
✓ Cost-Effective Solution - Lower initial investment than automated systems
✓ Flexible Operation - Adaptable to various tasks with operator control
✓ Simple Maintenance - Easier to repair with basic components
✓ Immediate Deployment - No programming needed for new tasks
B. For Automated Overhead Cranes:
✓ Precision Handling - ±1mm positioning accuracy
✓ 24/7 Operation - Continuous unmanned production
✓ Enhanced Safety - Built-in collision avoidance systems
✓ Data Integration - Connects with WMS/MES for smart manufacturing
Application:
Common Industrial Applications
A. Manufacturing:
Automotive: Engine/body panel positioning
Steel Mills: Coil and slab handling
Aerospace: Large component assembly
B. Warehousing & Logistics:
Container loading/unloading
High-bay storage retrieval
C. Construction & Heavy Industry:
Prefabricated concrete handling
Power plant equipment maintenance
D. Specialized Applications:
Cleanroom material transfer (pharmaceuticals)
Hazardous environment operations
Crane production procedure
1. Design and Engineering
Initial Consultation: The process begins with discussions between the manufacturer and the customer to understand the crane's operational requirements, such as load capacity, span, lifting height, and environment (e.g., indoor or outdoor use, temperature conditions, etc.).
Engineering & Customization: The design team customizes the crane, including the structure, lifting system, and radio remote control features. Detailed engineering drawings and specifications are prepared, ensuring the crane meets all required standards and safety codes.
Control System Design: The radio remote control system is integrated into the design, with attention to ease of use, range, safety features (emergency stop, overload protection), and compatibility with the crane's other systems.
2. Material Selection and Procurement
Structural Materials: High-quality materials like steel are sourced for the crane's main beam, girder, end carriages, and other structural components. These materials are selected for their strength, durability, and ability to withstand heavy loads.
Mechanical Components: The components for the hoisting system, trolley, crane wheel, motors, gearboxes, and radio remote control system are procured from reliable suppliers.
Electrical Components: Wiring, electrical panels, switches, safety devices, and other electrical components for the crane's control system are also sourced.
3. Fabrication and Manufacturing
Main Beam Construction: The steel is cut, welded, and assembled to form the main girder (single beam) of the crane. This process often involves precision cutting, bending, and welding to meet specific design tolerances.
End Carriage Fabrication: The end carriages, which support the crane's travel mechanism, are fabricated and assembled. These components are designed for stability and strength, ensuring smooth crane movement along the tracks.
Assembly of Lifting Mechanism: The hoist, hook, and lifting mechanism are assembled, with motors, gears, and pulleys integrated into the system. The lifting system is tested for load-bearing capacity and smooth operation.
Trolley and Crane Traveling Mechanisms: The trolley and crane traveling mechanisms are built and assembled. This includes the wheels, motor, and rail system, ensuring smooth movement of the crane along the rails.
Radio Remote Control Installation: The radio remote control system is installed. This includes fitting the necessary receivers, antennas, and integrating the control system with the crane's electrical and mechanical systems.
4. Electrical and Control System Integration
Wiring and Electrical Systems: The electrical wiring is installed, connecting the hoisting system, control panel, motors, and radio remote control system. The wiring is tested for safety and compliance with electrical codes.
Control Panel Assembly: The crane's control panel is assembled and integrated with the radio remote control system. It is tested for responsiveness and safety features, including emergency stop and overload protection.
Safety Features: Safety devices such as limit switches, overload sensors, and sound and light alarms are installed and integrated into the control system. These systems ensure safe crane operation and prevent damage.
5. Testing and Quality Control
Load Testing: The crane is subjected to a load test to ensure it can handle the specified weight capacity. The test is done using calibrated weights to verify the crane's performance under operational conditions.
Operational Testing: The crane undergoes a full operational test, where it is run through its motions (lifting, lowering, traveling, etc.) using the radio remote control. The crane's response to commands, including emergency stop and safety alarms, is closely monitored.
Electrical & Mechanical Testing: All electrical systems, including the radio remote control, are tested for functionality and safety. The motors, brakes, and electrical wiring are inspected for proper operation.
Inspection for Compliance: The crane is inspected for compliance with local and international standards (such as ISO, CE, or OSHA) to ensure it meets safety regulations. The structure, load-bearing components, and safety systems are thoroughly checked.
6. Final Assembly
Final Assembly and Inspection: After testing, the crane is fully assembled, with all components securely attached and double-checked for accuracy. The radio remote control is configured, and the system is tested one last time to ensure seamless integration.
Painting & Finishing: The crane is painted with protective coatings to prevent corrosion and improve its appearance. The final finishing touches are added to the structure, including any labeling or safety markings.
Documentation: All necessary documentation, including manuals, certificates of compliance, test reports, and warranty information, are prepared for the customer.

Workshop view:
The company has installed an intelligent equipment management platform, and has installed 310 sets (sets) of handling and welding robots. After the completion of the plan, there will be more than 500 sets (sets), and the equipment networking rate will reach 95%. 32 welding lines have been put into use, 50 are planned to be installed, and the automation rate of the entire product line has reached 85%.


Hot Tags: ld overhead crane, China ld overhead crane manufacturers, suppliers, factory, Single Girder Overhead Crane, Single Girder Overhead Travelling Crane
You Might Also Like



Send Inquiry