

How EPC Contractors Select Overhead Cranes for New Steel Plants
Most Important Takeaway (Read This First)
In a new steel plant project, EPC contractors select overhead cranes not simply by rated capacity, but by strict alignment with tender specifications, heavy-duty steel mill operating conditions, technical compliance, lifecycle reliability, and project schedule risk control-because a delayed or under-designed ladle crane can directly postpone plant commissioning and production startup.
Key Takeaways
Overhead crane selection for steel plants begins with detailed tender specification analysis, including duty classification, environmental conditions, and application-specific requirements.
Technical evaluation focuses on heavy-duty crane design, fatigue verification, heat resistance, redundancy, and integration with steel plant automation systems.
EPC contractors use structured technical bid evaluation and compliance matrices to compare crane manufacturers.
Project timeline risk is critical since ladle cranes, EAF cranes, and rolling mill cranes are long-lead equipment.
Interface risks with runway beams, civil structures, and electrical systems must be engineered early to prevent costly redesign.
Vendor selection balances total cost of ownership, manufacturing capability, and delivery reliability-not just initial crane price.
What Questions Are Solved in This Article?
How do EPC contractors evaluate overhead cranes for a new integrated steel plant?
What technical criteria are used in steel mill crane selection?
How do tender specifications influence crane design and procurement?
Why are ladle cranes and heavy-duty EOT cranes considered high-risk equipment in project schedules?
How do EPC contractors reduce delivery delay and commissioning risk?
The Role of Overhead Cranes in New Steel Plant Projects
Overhead cranes are production-critical systems in steel plants, integrated directly into the production flow. They handle molten steel, scrap, billets, slabs, and coils across all shifts, supporting melt shop, casting, and rolling mill operations.
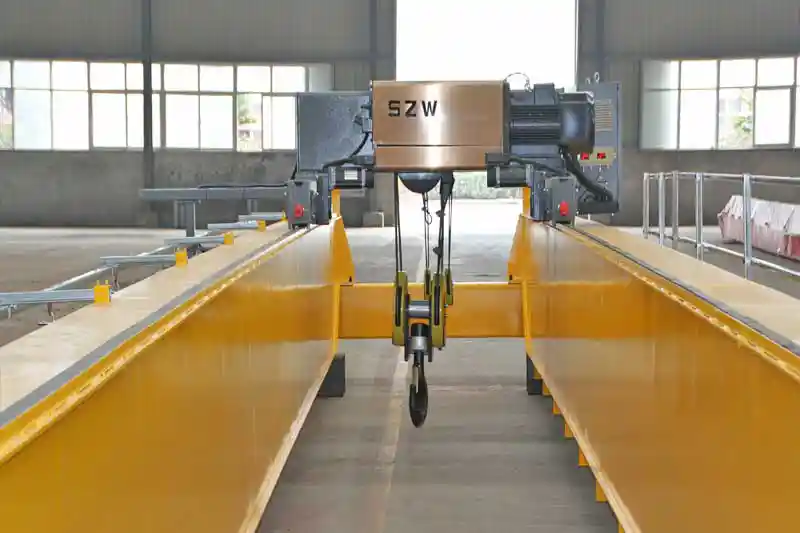
Overhead cranes for sale, tailored steel mill cranes for metal industrial sectors
Overhead Cranes Are Part of the Steel Production Process
In a new integrated steel plant, overhead cranes are not auxiliary equipment. They are built into the production flow. Whether the project uses a BOF (Basic Oxygen Furnace) route or an EAF (Electric Arc Furnace) process, heavy-duty overhead cranes handle molten steel, scrap, billets, slabs, and finished coils every day, every shift.
When a ladle crane moves, steel moves. When it stops, production waits. That's the reality inside a melt shop.
In practical terms, different areas of a steel plant require different types of EOT cranes:
Ladle handling cranes for transporting molten steel from furnace to ladle and to continuous casting
Scrap charging cranesequipped with grab buckets for EAF feeding
Tundish and billet handling cranes in the continuous casting bay
Slab and coil handling cranes in hot rolling and cold rolling mills
Maintenance cranes for servicing heavy equipment
Each crane is engineered according to its task, load spectrum, and duty cycle. There is no "standard" solution that fits all areas.
Steel Plant Operating Conditions Define Crane Design
Overhead cranes in steel mills operate in conditions far more demanding than general manufacturing facilities. Design choices are driven by environment, load frequency, and safety requirements.
High Ambient Temperature and Radiant Heat
In BOF and EAF melt shops, ambient temperatures can be high, especially near furnaces and ladles. Radiant heat from molten steel adds further stress to motors, brakes, and electrical panels.
Steel mill overhead cranes in these zones typically include:
Heat-resistant hoist motors with higher insulation class
Thermal shielding for electrical control panels
High-temperature wire ropes
Protected brake systems and insulated cab design (if cabin-operated)
Without these measures, overheating and insulation breakdown are common failure points.
Dust, Fumes, and Corrosive Environment
EAF operations generate metallic dust and fine particles that settle on mechanical and electrical components. Rolling mills add scale and oil mist to the mix.
To maintain reliability, steel plant crane specifications often require:
IP54 or higher protection for electrical enclosures
Sealed braking systems
Enclosed gearboxes with controlled lubrication
Industrial-grade anti-corrosion coating systems
These are not upgrades. They are baseline requirements for long service life in steel production environments.
High-Duty Cycle and Fatigue Requirements
Steel production rarely pauses. Many overhead cranes operate across three shifts with continuous lifting cycles. Because of this, tender documents usually specify:
FEM A7 or A8 duty classification
CMAA Class E or Class F service rating
Fatigue design verification based on load spectrum
High service factor for hoisting mechanisms
This means structural girders, end carriages, wheels, and gearboxes must withstand millions of load cycles. Fatigue life calculation and wheel load analysis are standard engineering checks in new steel plant projects.
Continuous Operation and Safety Redundancy
In molten metal handling, safety is not optional. A mechanical or braking failure during ladle lifting can have serious consequences.
For ladle cranes and other critical steel mill cranes, EPC specifications often include:
Dual hoisting mechanisms
Independent drive systems
Redundant braking systems
Emergency stop and overload protection
Load monitoring systems
Redundancy is built into the design to reduce operational risk and improve reliability.
Why EPC Contractors Treat Crane Procurement as a Strategic Decision
In new steel plant construction, overhead cranes are long-lead items. Design finalization, fabrication, assembly, and factory testing can take several months. A delay in crane delivery can affect runway installation, mechanical completion, and hot commissioning.
Because of this, EPC contractors manage crane selection and procurement carefully, focusing on:
Early confirmation of crane capacity, span, and wheel loads
Coordination with civil and structural teams for runway beam design
Detailed review of technical specifications and duty classification
Factory acceptance testing before shipment
Manufacturing progress monitoring against project schedule
Crane procurement is directly linked to project timeline control.
Practical Alignment with Steel Plant Design
The selection of an overhead crane in a new steel plant must align with:
Furnace size and ladle capacity
Annual production output targets
Building span and runway beam structure
Automation system integration
Maintenance access and spare parts strategy
In short, overhead cranes in steel plants are production-critical systems. They operate under heat, dust, high load cycles, and tight schedules. That is why EPC contractors evaluate them with the same level of attention as furnaces, casting machines, and rolling mills.
Tender Specifications: The Foundation of Crane Selection
In a new steel plant project, the tender specification is the starting point for selecting an overhead crane. EPC contractors do not begin with price. They begin with compliance.
The crane must meet every technical requirement written in the EPC tender package. If it does not, it will not pass technical evaluation. It's that straightforward.
Technical Tender Requirements for Steel Mill Cranes
The technical specification defines how the overhead crane must perform and under what conditions it must operate. These are clear engineering inputs, not suggestions.
Common requirements include:
Rated lifting capacity for main and auxiliary hoists
Crane span and lifting height, based on building layout
Hook approach limits to ensure full coverage of the working area
Duty classification (ISO, FEM, CMAA)
Load spectrum and fatigue life design criteria
Seismic and structural design parameters
Environmental requirements, such as heat-resistant design and IP protection class
Each item affects crane structure, motor size, gearbox selection, and braking system.
For example, a ladle crane used for molten steel handling in a BOF or EAF shop must typically include:
Dual hoisting mechanisms
Redundant braking systems
Heat-protected electrical panels
High-temperature resistant wire ropes
Overload protection and emergency stop systems
These features are not optional upgrades. They are required for safety and compliance in steel mill applications.
Compliance with International Standards
EPC contractors verify that the proposed overhead crane meets recognized international standards. This ensures structural strength, fatigue resistance, and operational safety.
Typical standards referenced in steel plant projects include:
FEM standards for structural fatigue verification
ISO crane safety standards
CMAA Class E or F duty ratings for heavy-duty service
Local safety and regulatory codes
If a supplier proposes a lower duty classification or reduced safety factor, it must be declared clearly. In most steel plant projects, such deviations are not accepted.
Simply put, compliance is not negotiable.
Documentation and Engineering Submittals
Technical claims must be supported by clear documentation. A qualified overhead crane manufacturer is expected to submit complete engineering data during the tender stage.
Typical required documents include:
General arrangement drawings (GA drawings)
Wheel load calculations for runway beam design
Structural analysis or FEA reports
Motor and gearbox datasheets
Electrical single-line diagrams
QA/QC plans
Factory Acceptance Test (FAT) procedures
Wheel load data is especially important because civil and structural teams use it to design runway beams and building columns.
If documents are missing or unclear, it creates risk for the EPC contractor. In many cases, incomplete submissions result in clarification requests or technical rejection.
In steel plant overhead crane procurement, the tender specification sets the rules. Technical compliance, proven through proper documentation, determines whether a supplier moves forward in the evaluation process.
Technical Evaluation of Overhead Cranes for Steel Plants
Once a crane passes the tender compliance stage, EPC contractors move to detailed technical evaluation. This is where drawings, calculations, and real engineering capability are examined closely.
Not all cranes in a steel plant are treated the same. A ladle handling crane in the melt shop carries far higher operational risk than a maintenance crane. Because of that, each crane type is evaluated according to its specific function and working conditions.
Application-Specific Crane Engineering
Different areas of a steel plant require different overhead crane configurations. EPC engineers assess each crane based on its operational role, load profile, and safety exposure.
Ladle Handling Cranes (Melt Shop)
Ladle cranes handle molten steel. The load is heavy, hot, and potentially dangerous. There is no tolerance for mechanical failure.
Technical evaluation typically focuses on:
Dual hoist systems for molten metal handling
Independent drive mechanisms for added reliability
Heat-resistant wire ropes and insulation systems
Redundant braking systems on each hoist
Emergency stop and overload protection systems
Engineers also review hoist speed control and synchronization between dual drums. Uneven lifting in molten metal handling is not acceptable.
If a ladle crane fails, production stops immediately. Worse, it may create serious safety hazards. That is why this category receives the most scrutiny.
Continuous Casting Cranes
Cranes in the continuous casting bay must operate with precision. They handle tundishes, billets, and slabs while working alongside automated casting equipment.
Evaluation usually includes:
High positioning accuracy for hoisting and trolley travel
Smooth VFD (Variable Frequency Drive) control
Controlled acceleration and deceleration
Integration with casting process automation systems
Jerky motion or poor speed control can disrupt casting operations. In this area, motion stability matters just as much as lifting capacity.
Rolling Mill and Coil Handling Cranes
In rolling mills, cranes handle finished coils and slabs. The pace is fast. Placement must be accurate.
Technical checks focus on:
High-speed cross travel capability
C-hook, tong, or specialized lifting attachments
Anti-sway control systems for precise coil positioning
Reliable braking under frequent travel cycles
Here, productivity and control stability are key. Small positioning errors can slow down downstream logistics.
Each crane type is reviewed separately. EPC contractors assess design safety, fatigue life, and operational risk based on how critical the crane is to steel production.
Mechanical System Evaluation
After application review, EPC engineers examine the mechanical design of the heavy-duty EOT crane in detail. The goal is simple: ensure the crane can run continuously without premature wear or failure.
Key mechanical checks include:
Gearbox service factor and hardened gear design
Wire rope safety factor and drum grooving design
End carriage wheel load distribution and bearing selection
Fatigue life verification under high load cycles
Structural welding quality and NDT (Non-Destructive Testing) compliance
Wheel loads are cross-checked against runway beam capacity. Gearbox ratings are compared with duty classification. Weld inspection records are reviewed carefully.
In steel mill applications, mechanical durability directly affects plant uptime. A gearbox failure during peak production is costly. EPC engineers look for proven design, not experimental solutions.
Electrical and Automation Integration
Modern steel plant overhead cranes are no longer standalone systems. They are integrated into plant-wide electrical and automation networks.
Technical evaluation includes:
VFD-controlled hoisting, trolley, and bridge travel drives
PLC-based crane control panels
Integration capability with SCADA or MES systems
Load monitoring and condition monitoring systems
SIL-rated safety circuits where required
Drive performance is reviewed for smooth acceleration, stable speed control, and safe braking. Starting current and power supply compatibility are also checked.
Electrical reliability is critical in steel production. If a hoist motor trips or a control system fails, the entire production line may stop. That risk is taken seriously during evaluation.
In short, technical evaluation goes beyond checking capacity and span. EPC contractors assess how the overhead crane will perform under real steel plant conditions-heat, dust, high load cycles, and continuous operation. The focus is durability, safety, and reliable integration into the production system.
Project Timeline Risk and Long-Lead Equipment Management
In a new steel plant project, schedule control is everything. Furnaces, casting machines, and rolling mills are all tied to a master construction timeline. Heavy-duty overhead cranes sit directly on that critical path.
If the crane is late, commissioning is late. There's no workaround for that.
Overhead Cranes as Critical Path Equipment
In EPC steel plant construction schedules, ladle cranes, melt shop cranes, and high-capacity double girder overhead cranes are classified as long-lead equipment. Manufacturing is not quick. Depending on lifting capacity, span, and customization, lead time typically ranges from 4 to 8 months, sometimes longer for large ladle handling cranes.
Several factors can cause delays:
Motor and gearbox procurement, especially for high-duty rated components
Structural fabrication bottlenecks in large-capacity girder production
Electrical component shortages, including VFDs and PLC modules
International logistics disruptions, particularly for oversized loads
A delayed ladle crane directly affects:
Runway beam load testing
Mechanical completion milestones
Hot commissioning of the melt shop
First steel tapping schedule
In practical terms, molten steel cannot move without a certified and tested crane. That's why EPC contractors closely monitor crane manufacturing progress from day one.
Civil and Structural Interface Risks
Overhead crane design is tightly connected to the building structure. Wheel loads, impact factors, and horizontal forces are used by civil engineers to design runway beams and supporting columns.
If crane parameters change after civil construction begins, the impact can be serious.
Possible consequences include:
Runway beam reinforcement or redesign
Column strengthening or replacement
Increased structural steel cost
Construction rework and schedule delay
Even a small increase in wheel load can affect beam sizing and foundation calculations.
To reduce this risk, EPC contractors require:
Early confirmation of crane capacity and span
Finalized wheel load calculations before structural steel fabrication
Clear approval of general arrangement drawings
Formal engineering freeze before procurement release
Early coordination between crane supplier and civil design team prevents costly late-stage changes.
Manufacturing and Quality Control Risk
Beyond schedule, EPC contractors evaluate manufacturing reliability. A supplier may offer competitive pricing, but if production capacity or quality control is weak, project risk increases.
Key evaluation points include:
Factory production capacity and workload planning
Certified welding procedures and welder qualifications
NDT (Non-Destructive Testing) procedures for structural welds
Gearbox and motor supplier traceability
Factory Acceptance Test (FAT) protocols
Delivery milestone tracking and reporting system
FAT is especially important. During Factory Acceptance Testing, EPC representatives verify:
Hoisting and travel performance
Brake functionality
Limit switch operation
Electrical control logic
Load testing under rated capacity
Witnessing FAT before shipment reduces installation and commissioning risk at site. It is far easier to correct issues in the factory than inside a completed steel plant building.
In steel plant projects, overhead cranes are not just equipment purchases. They are schedule-sensitive, structure-dependent, heavy-duty systems. Managing lead time, engineering interfaces, and manufacturing quality is essential to protect the overall project timeline and ensure safe commissioning.
Commercial Evaluation and Total Cost of Ownership
Price matters. Everyone knows that. But in a new steel plant project, EPC contractors do not select an overhead crane based on purchase price alone. They look at the total cost of ownership over the crane's operating life.
A steel mill crane may run for 15 to 25 years under high-duty conditions. Over that period, maintenance cost, downtime risk, and spare parts supply often exceed the initial capital cost.
Looking Beyond the Initial Crane Price
During commercial evaluation, EPC teams assess long-term operating impact. The focus shifts from "How much does it cost today?" to "What will it cost to run and maintain?"
Key factors typically reviewed include:
Lifecycle maintenance cost, including wear parts and overhaul intervals
Spare parts availability and lead time
Local service capability and technical support response time
Mean Time Between Failures (MTBF) data for critical components
Energy efficiency of hoist motors and VFD drive systems
For example, a ladle handling crane operating in a melt shop cannot afford frequent gearbox or brake replacements. If spare parts require long international shipping times, downtime increases. In a high-output steel plant, one day of lost production can cost far more than any initial price difference.
Reliability and Downtime Cost in Steel Mills
In continuous steel production, overhead crane reliability directly affects output. A lower-priced crane with undersized components or lower duty classification may appear competitive during bidding. But if it experiences repeated breakdowns, the real cost becomes visible quickly.
Operational cost drivers include:
Unplanned downtime due to hoist motor or brake failure
Frequent wire rope replacement under high load cycles
Gearbox overheating or lubrication issues
Electrical faults in control panels or VFD systems
Each interruption affects furnace scheduling, casting rhythm, and rolling mill logistics. Over time, poor reliability translates into higher operating expense.
Vendor Scoring and Evaluation Matrix
To balance technical performance and commercial competitiveness, EPC contractors typically use a weighted evaluation matrix. This structured approach reduces subjective decision-making.
The scoring model often includes:
Technical compliance score
Duty classification and fatigue design verification
Manufacturing capability assessment
Delivery schedule commitment
Commercial price comparison
Service and spare parts support rating
Each category is assigned a weight based on project priorities. For melt shop cranes, technical reliability and safety usually carry higher weight than minor price differences.
This method allows EPC contractors to select a crane supplier based on risk-adjusted value, not just the lowest bid.
Operational Reality Drives Commercial Decisions
In steel plant overhead crane procurement, commercial evaluation is closely tied to operational reality. The goal is not simply to buy a crane at a lower price. The goal is to secure a heavy-duty crane system that delivers stable performance, manageable maintenance cost, and long-term reliability under demanding steel mill conditions.
Final Vendor Selection and Approval
Selecting the right overhead crane supplier is the final, but critical, step in the EPC process. By this stage, technical evaluation, tender compliance, and commercial assessment are complete. The goal is to identify a supplier who can deliver a crane that performs reliably in the harsh conditions of a steel plant, on time, and within budget.
Key Factors in Vendor Selection
EPC contractors typically consider several practical criteria when making the final decision:
Full technical compliance with tender specifications, including duty class, lifting capacity, span, and environmental requirements
Proven experience in delivering heavy-duty steel mill cranes, such as ladle handling, continuous casting, and rolling mill cranes
Demonstrated manufacturing capability, including production capacity, QA/QC processes, and welding standards
Delivery schedule reliability, ensuring the crane will be completed and shipped in line with project timelines
Competitive lifecycle value, factoring in maintenance cost, spare parts availability, and expected reliability over years of operation
Each of these factors is weighed together to minimize project risk and ensure smooth commissioning.
Procurement and Approval Process
Even after a supplier is selected, the crane is not immediately manufactured. EPC contractors require:
Client approval confirming technical and commercial acceptance
Engineering sign-off verifying all design details, load calculations, and integration with civil and structural work
Only after these approvals does procurement release the order to the manufacturer. This step ensures that the crane meets project requirements, aligns with construction schedules, and reduces the risk of late-stage design changes.
Summary
In short, the final vendor selection is a careful balance of technical capability, manufacturing reliability, schedule certainty, and long-term operational value. Choosing the right supplier ensures that the overhead crane will support safe, efficient, and uninterrupted steel plant operations.
Frequently Asked Questions (FAQ) – Overhead Crane Selection in New Steel Plants
Q1: How do EPC contractors evaluate overhead cranes?
A: EPC contractors follow a structured process. They start by reviewing tender specifications, then evaluate the crane's mechanical, electrical, and automation design. Each crane type is assessed based on its function-ladle cranes, casting cranes, and rolling mill cranes all have different operational risks. The evaluation ensures the crane can perform reliably under high temperature, heavy-duty cycles, and continuous production conditions.
Q2: What technical criteria are used in steel mill crane selection?
A: Technical evaluation focuses on real-world operational performance. Key criteria include:
Lifting capacity for main and auxiliary hoists
Duty classification (FEM, CMAA, ISO)
Fatigue life and load spectrum verification
Environmental resistance (heat, dust, IP protection)
Redundancy and safety systems (dual hoists, brakes, emergency stops)
Integration with plant automation and control systems
Each criterion is assessed to ensure safety, reliability, and smooth production flow.
Q3: How do tender specifications influence crane design and procurement?
A: Tender specifications set the rules for design and compliance. They define:
Rated load and span
Hook approach limits
Duty classification and fatigue requirements
Seismic and structural parameters
Environmental protection requirements
Suppliers must meet these specifications fully. Deviations can lead to technical rejection. Clear, detailed tender documents also allow EPC teams to coordinate civil, structural, and electrical work early.
Q4: Why are ladle cranes and heavy-duty EOT cranes high-risk in schedules?
A: These cranes are long-lead, critical-path items. Manufacturing can take 4–8 months or more. Delays in crane delivery affect:
Runway beam load testing
Mechanical completion milestones
Hot commissioning and first steel tapping
Because they handle molten steel or large billets, operational failure is not an option. Any delay directly impacts the overall plant schedule.
Q5: How do EPC contractors reduce delivery delays and commissioning risk?
A: Risk mitigation strategies include:
Early engineering freeze and wheel load confirmation
Detailed review of technical specifications before procurement
Factory Acceptance Testing (FAT) before shipment
Tracking manufacturing milestones and supplier reliability
Selecting vendors with proven experience in steel mill crane projects
These measures ensure cranes arrive on time, meet design requirements, and integrate smoothly into plant operations.
Conclusion
Selecting overhead cranes for a new steel plant is more than buying lifting equipment-it is a multidisciplinary process that combines engineering, risk management, and project planning. EPC contractors must ensure full compliance with tender specifications while verifying that cranes can withstand the demanding conditions of a steel mill.
Ladle cranes, EAF cranes, rolling mill cranes, and other heavy-duty overhead cranes are production-critical systems, not standard material handling tools. Their performance directly affects plant commissioning, operational safety, and long-term output.
Success in crane selection requires:
Thorough technical evaluation of mechanical, electrical, and automation systems
Early coordination with civil and structural engineering teams to confirm wheel loads and runway requirements
Rigorous quality control and Factory Acceptance Testing (FAT)
Careful management of long-lead manufacturing and delivery risks
In high-capacity steel plants, choosing the right crane supplier is essential. The correct overhead crane system ensures safe, reliable operation, protects the production schedule, and supports long-term plant efficiency.


